English
 Español
 Português
 Русский
 العربية
 Français
 Deutsch
 中文
 日本語
 한국어


Endoscope Waterproof Connectors and Assembly Components
Designed for multi-pin waterproof connectors, cable interfaces and coordinated endoscope subassemblies, these custom-molded components combine functional geometry with production-ready part design. The molding plan is developed around accurate pin and connector alignment, stable sealing grooves and overmold interfaces, and protected cable routing through assembled components. Resin selection, gate location, parting lines and inspection points are matched to the mating parts, operating environment and expected production volume.
Product Overview
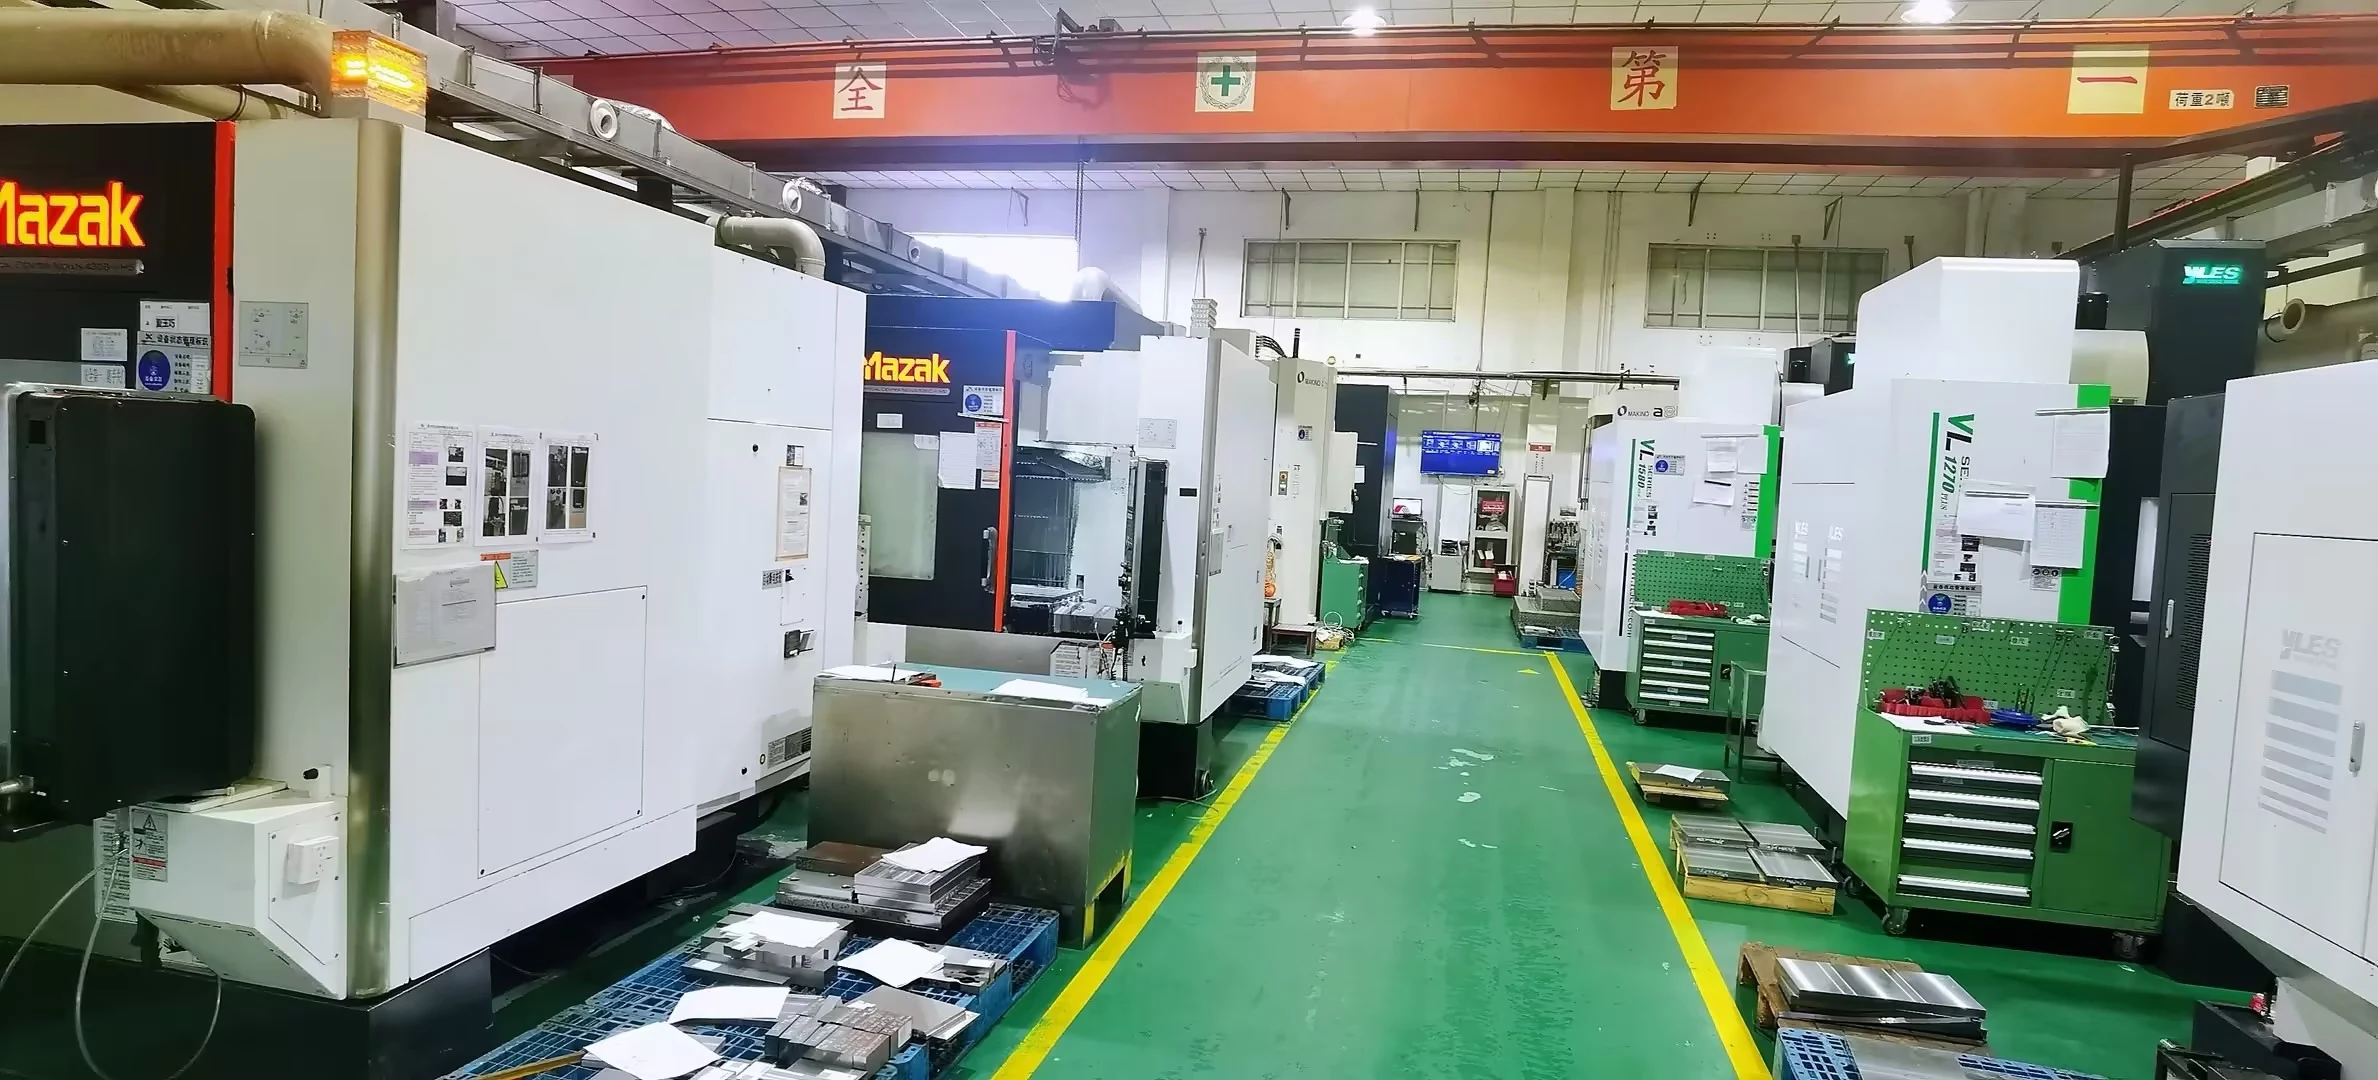
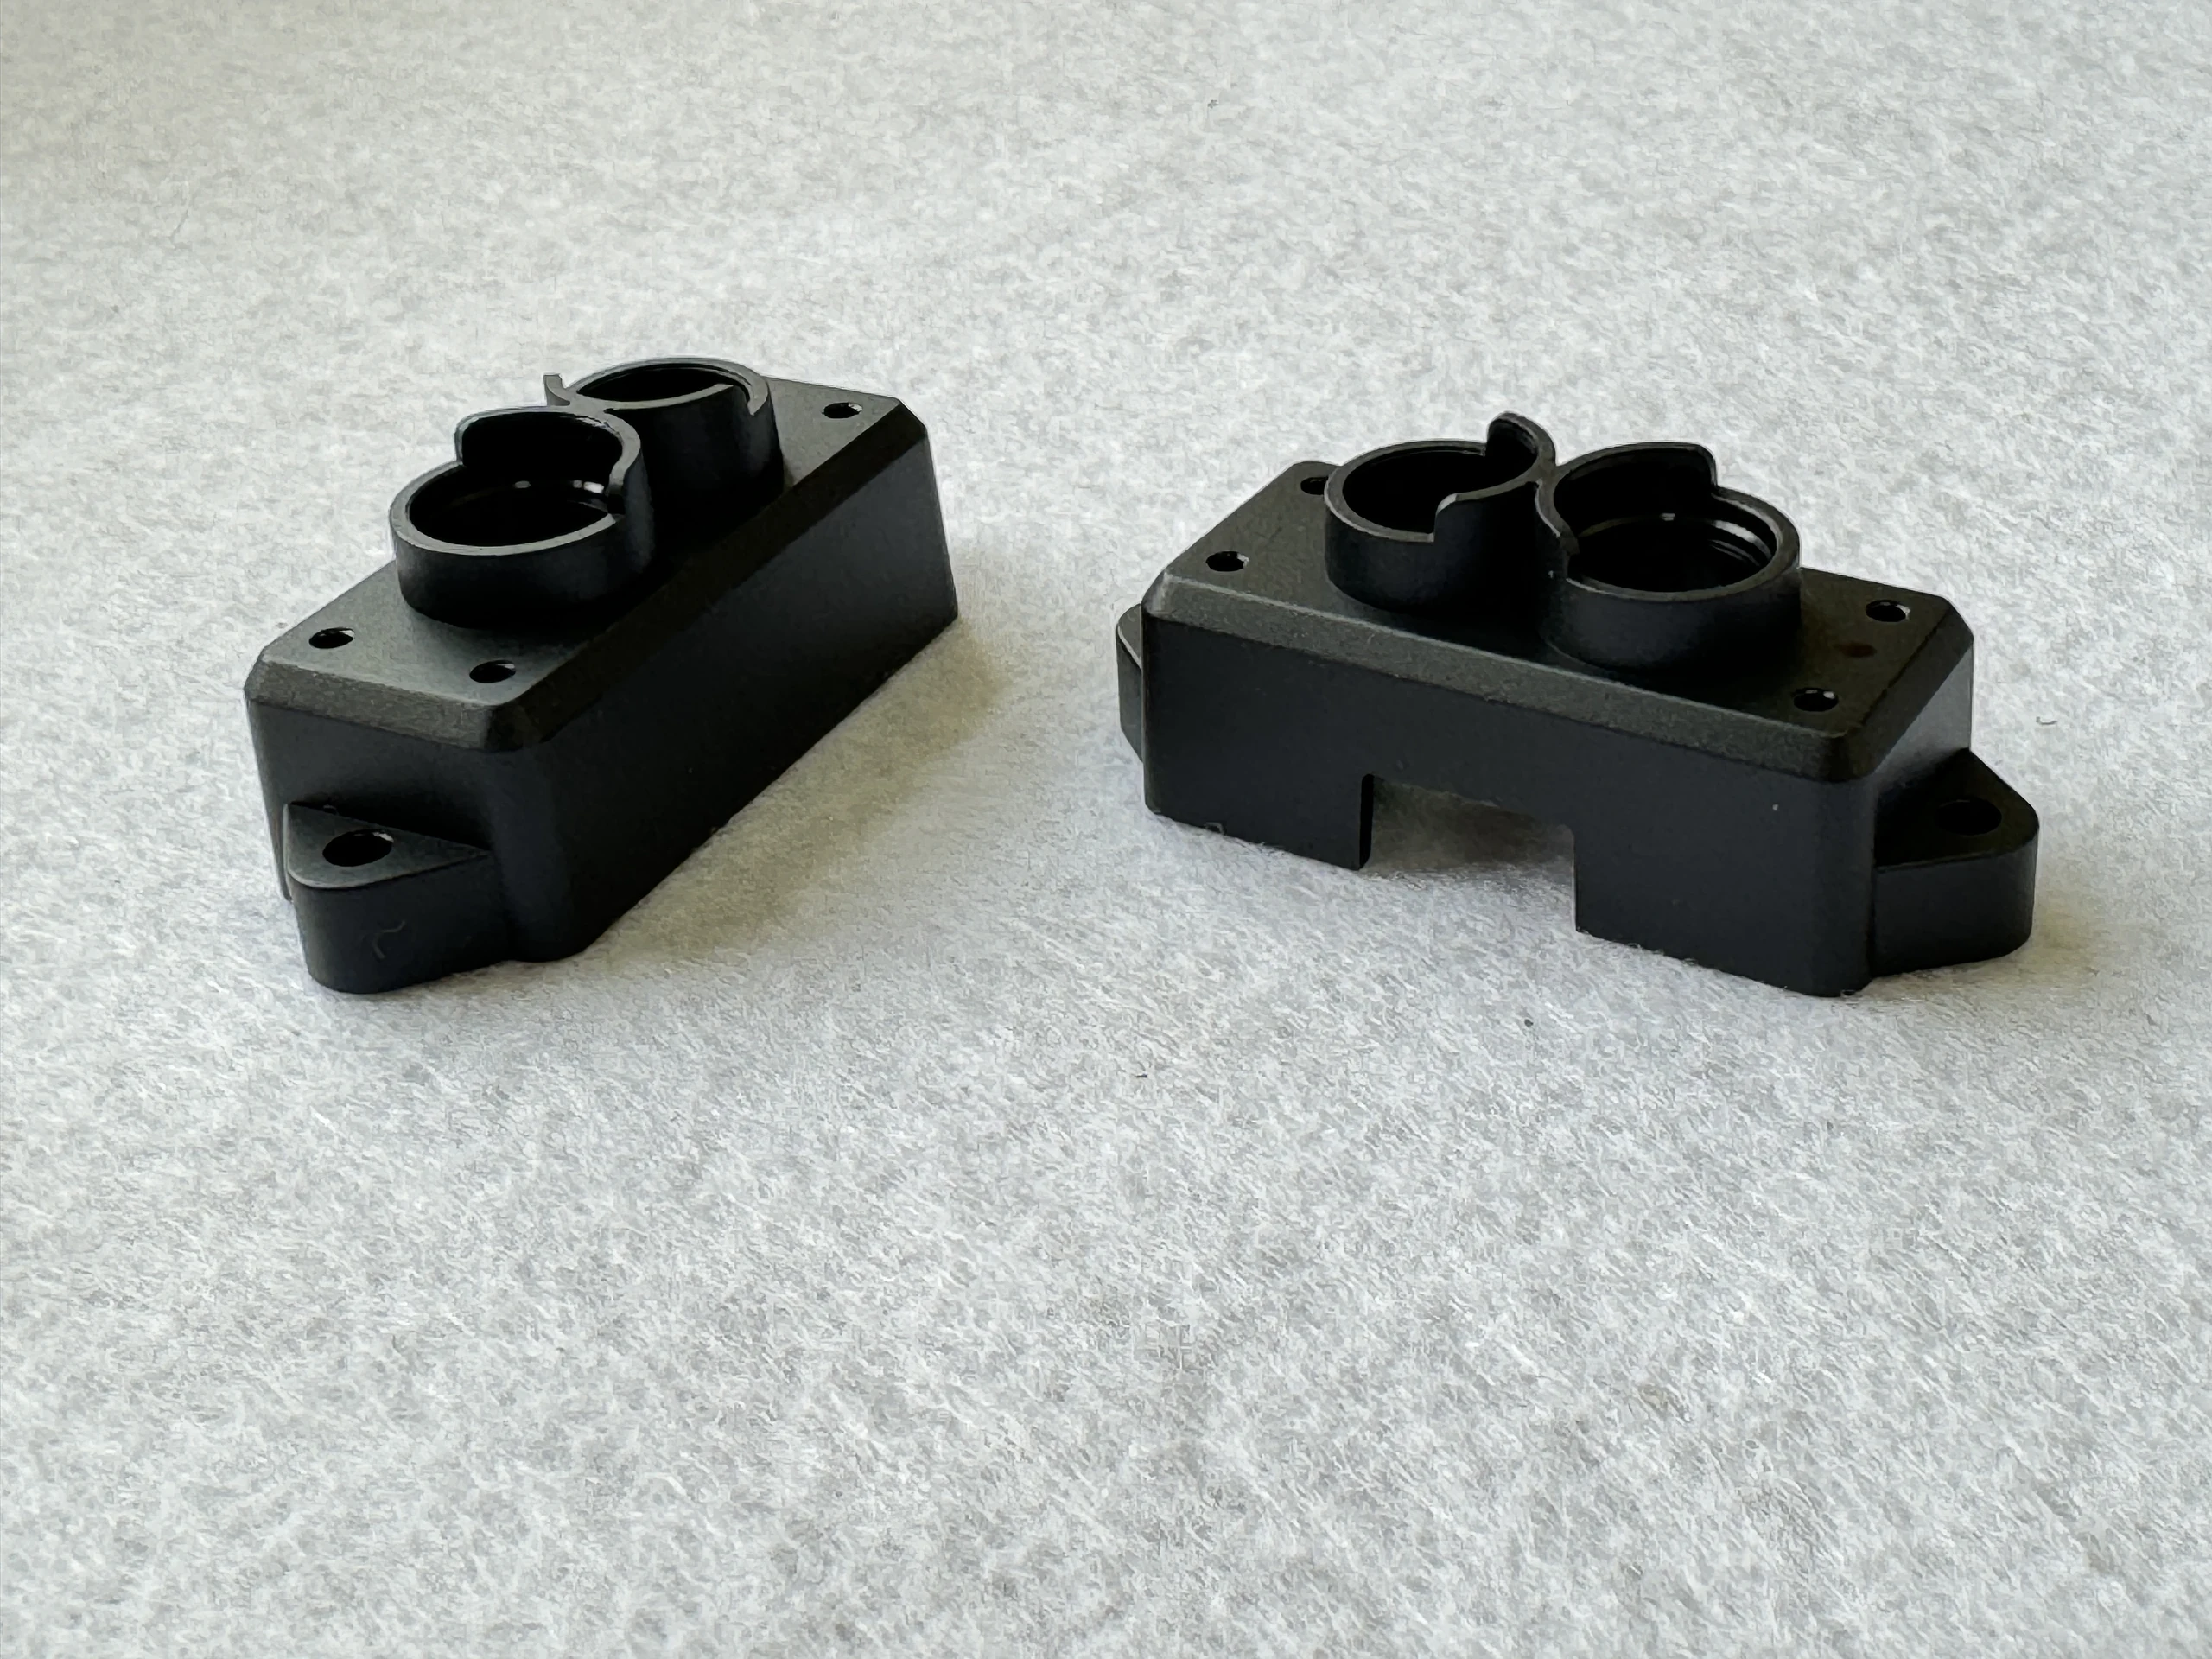
Endoscope connector components bring together locating features, seal interfaces and assembly clearances in a compact part. JingZhan develops the tooling and moulding process around the customer’s connector design and mating components. The word waterproof describes the intended assembly function, not a certified rating for every pictured item. Seal performance must be established through a defined assembled-product test. DESIGN AND MANUFACTURING Identify the faces and diameters that locate or compress a seal. Agree surface condition, allowable flash and dimensional acceptance at these locations. Include the actual seal, counterpart and fastening method in trial reviews rather than judging the moulded housing in isolation. Check hole locations, connector cavities and any insert seats against the assembly stack. Where inserts are required, specify their material, retention and supply responsibility. Insert moulding or secondary installation is evaluated and quoted separately instead of assumed from a photograph. Review gates, vents and wall transitions around openings and ribs. Keep weld lines and ejector marks away from agreed critical areas where practicable. Trial samples should be examined for short shots, burrs, distortion and features that could obstruct assembly. Provide the intended cleaning chemistry, temperature, pressure and exposure duration. Define any leak test, test fixture and pass criteria before qualification. No IP grade, immersion life or sterilisation compatibility is assigned without supporting project evidence. TECHNICAL SPECIFICATIONS PRODUCTION AND REPEAT SUPPLY Tooling support can use CNC machining and EDM for cavity details, followed by injection moulding on a machine selected from the supplied 50–500-tonne equipment range. CMM or optical checks can be planned for locating and seal features. Dedicated leak or functional testing requires a separately agreed fixture, procedure and responsibility; the equipment list alone does not establish that validation. Agree the drawing revision, resin grade, approved samples and critical-to-quality features before release. Record material lots and moulding conditions, inspect first-off parts and use cavity identification where specified. Define packaging, sampling and change approval so later deliveries can be compared with the same baseline. Tool maintenance and replacement inserts should be planned around actual production demand. Tooling investment is quoted separately from the piece price. Share annual demand and release quantities so cavity count, procurement and batch cost can be reviewed together. RELATED APPLICATIONS Connector housings and interface bodies within customer-designed electronic endoscope assemblies. Instrument cable and module interfaces requiring repeatable positioning and controlled seal contact geometry. Related inspection-system connectors and plastic interface parts, subject to their own environmental requirements. These photographs show manufactured component examples, not finished medical devices. Medical suitability, biocompatibility, cleaning or sterilisation compatibility and device approval require a defined project scope and customer validation; they are not implied by appearance or resin name. Discuss your drawing and supply requirements. Send CAD, resin preference, critical features, annual demand and release quantity. Contact our engineering team →Connector components developed for controlled fit and sealing interfaces
Key processing requirements
Seal lands and mating geometry
Openings and insert position
Filling around complex sections
Validation based on the actual exposure
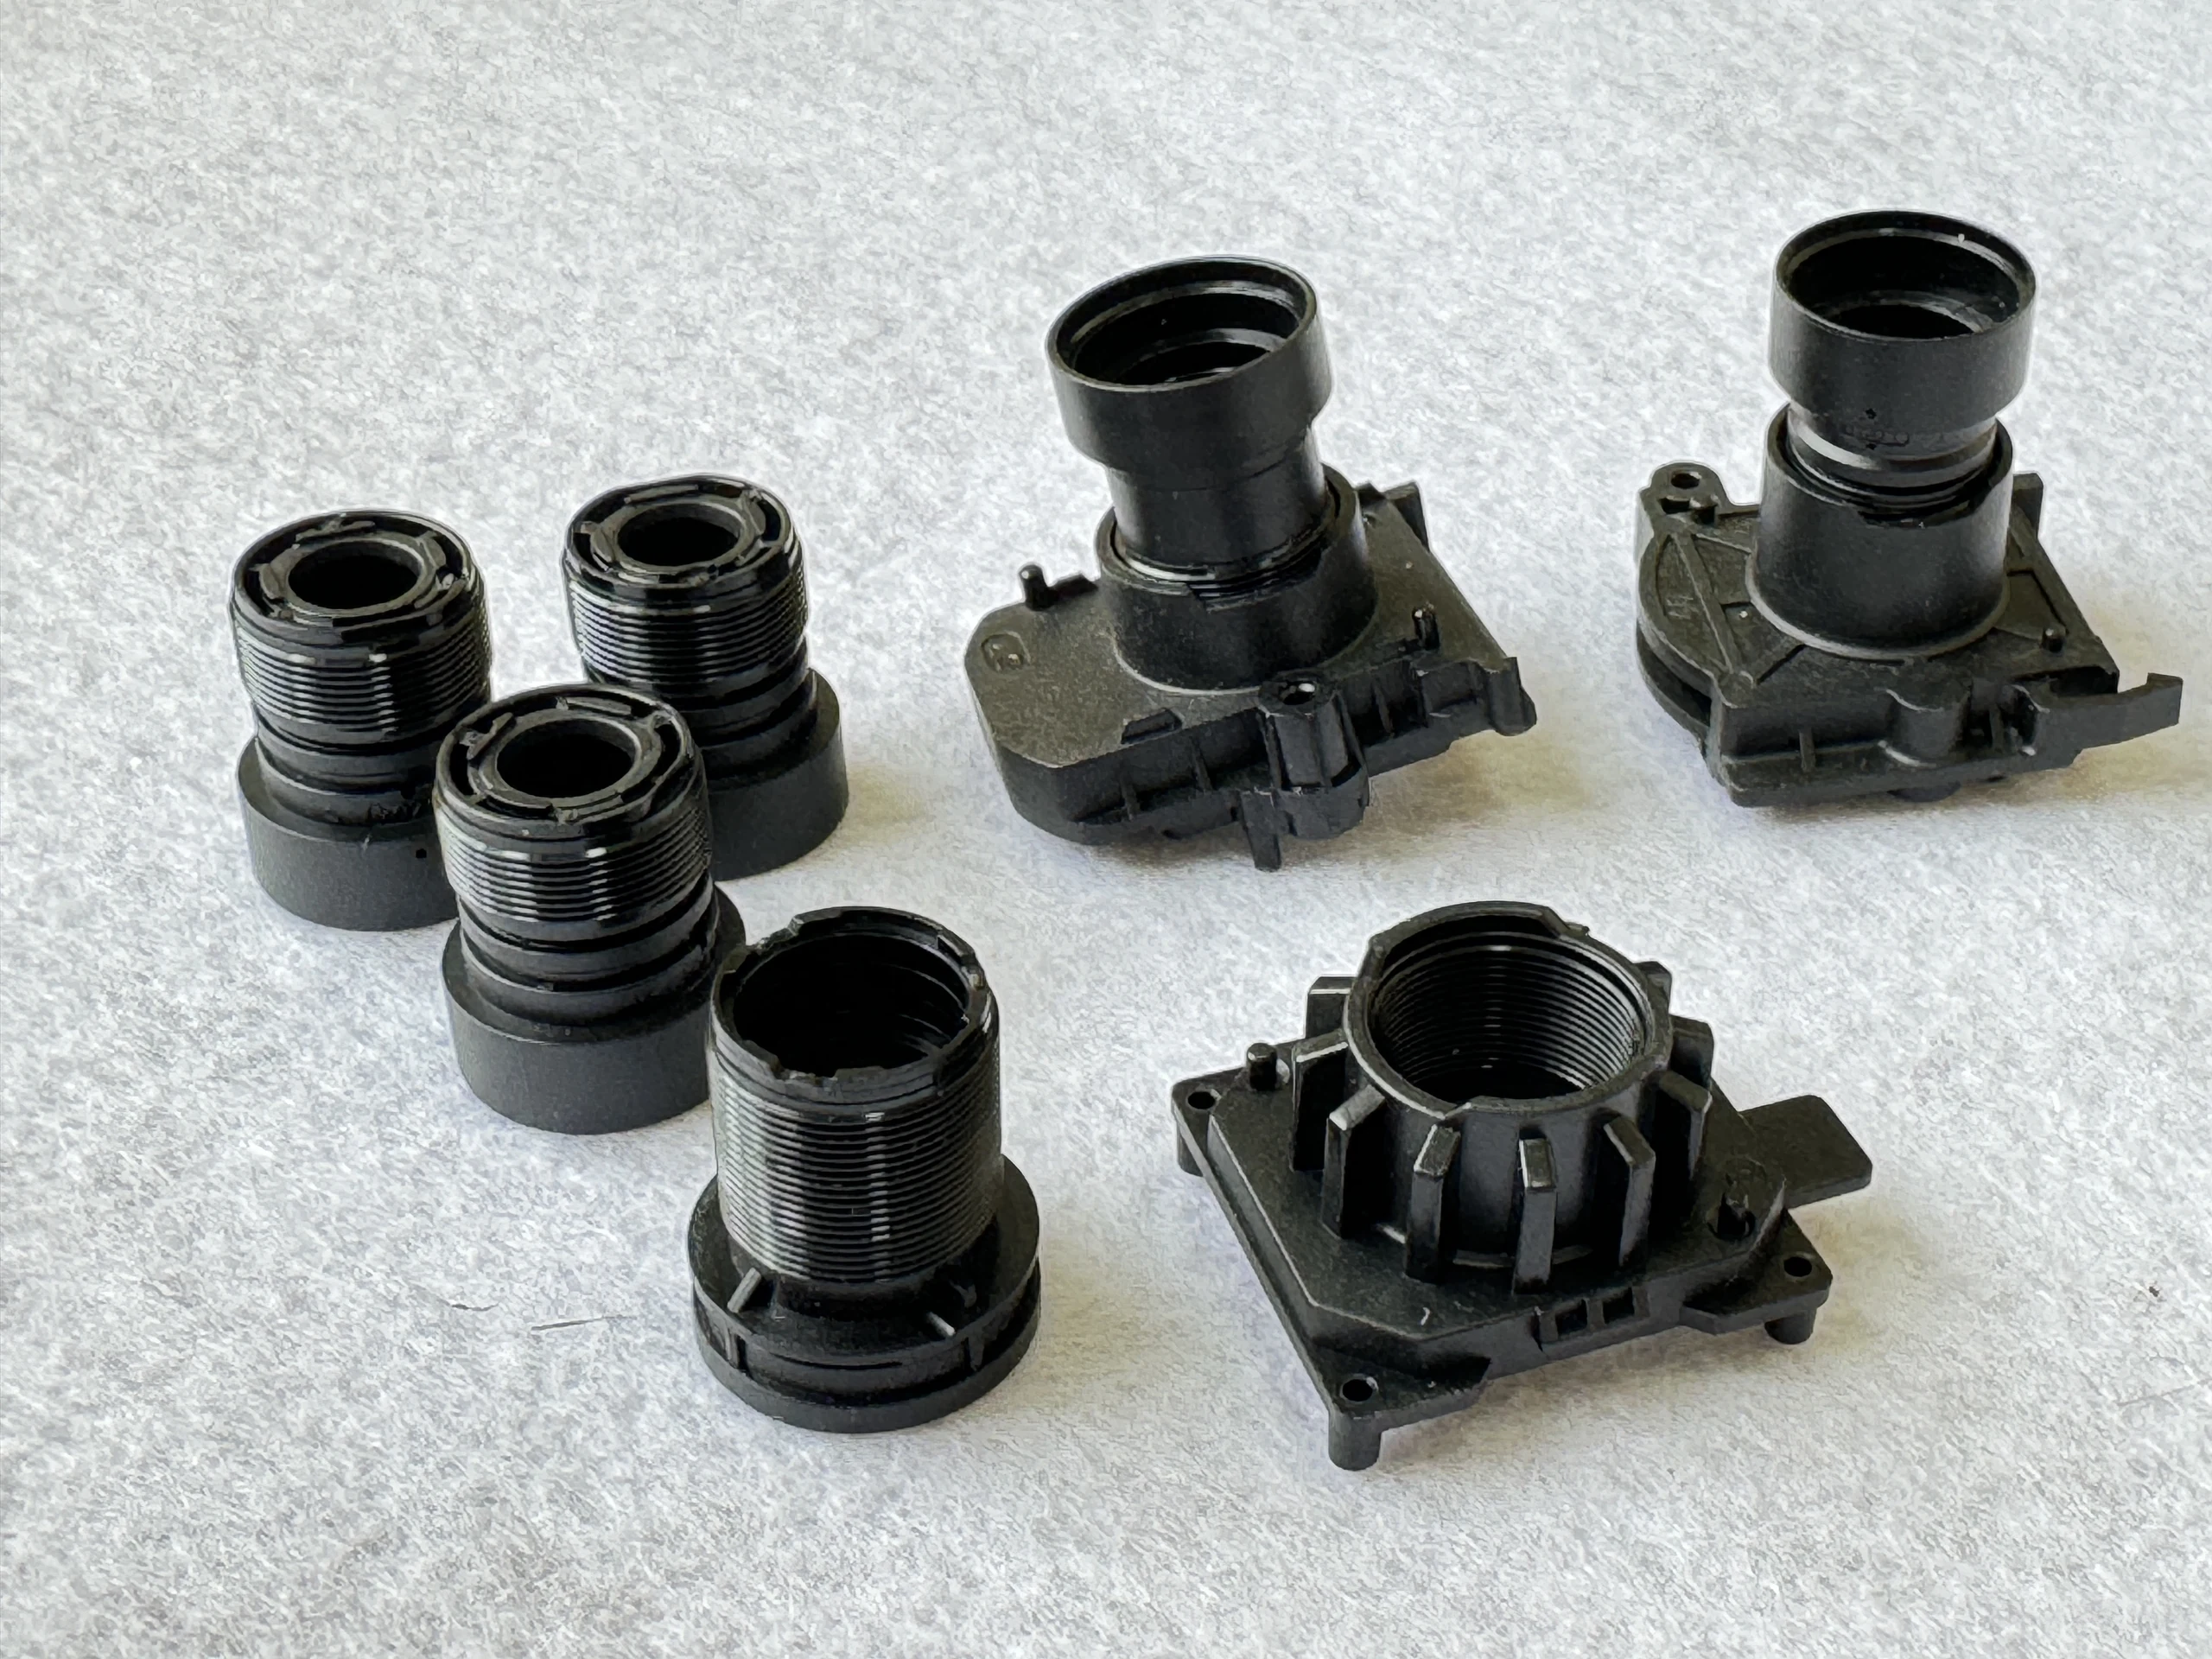
Parameters agreed for your part
Parameter
Project specification
Process scope
Custom moulded connector bodies and associated plastic assembly components.
Resin grade
Engineering resin selected against mechanical, chemical and dimensional needs.
Sealing interfaces
Customer-defined seal lands, grooves and counterpart geometry.
Connector layout
Number, position and dimensions of openings to approved CAD.
Insert requirements
Material, position and retention agreed; additional operations separately scoped.
Tolerances
Specified by feature, with datum system and inspection method.
Leak-test scope
Test conditions and acceptance criteria defined for the assembled design.
Packaging
Protection for seal surfaces, contact areas and identified component sets.
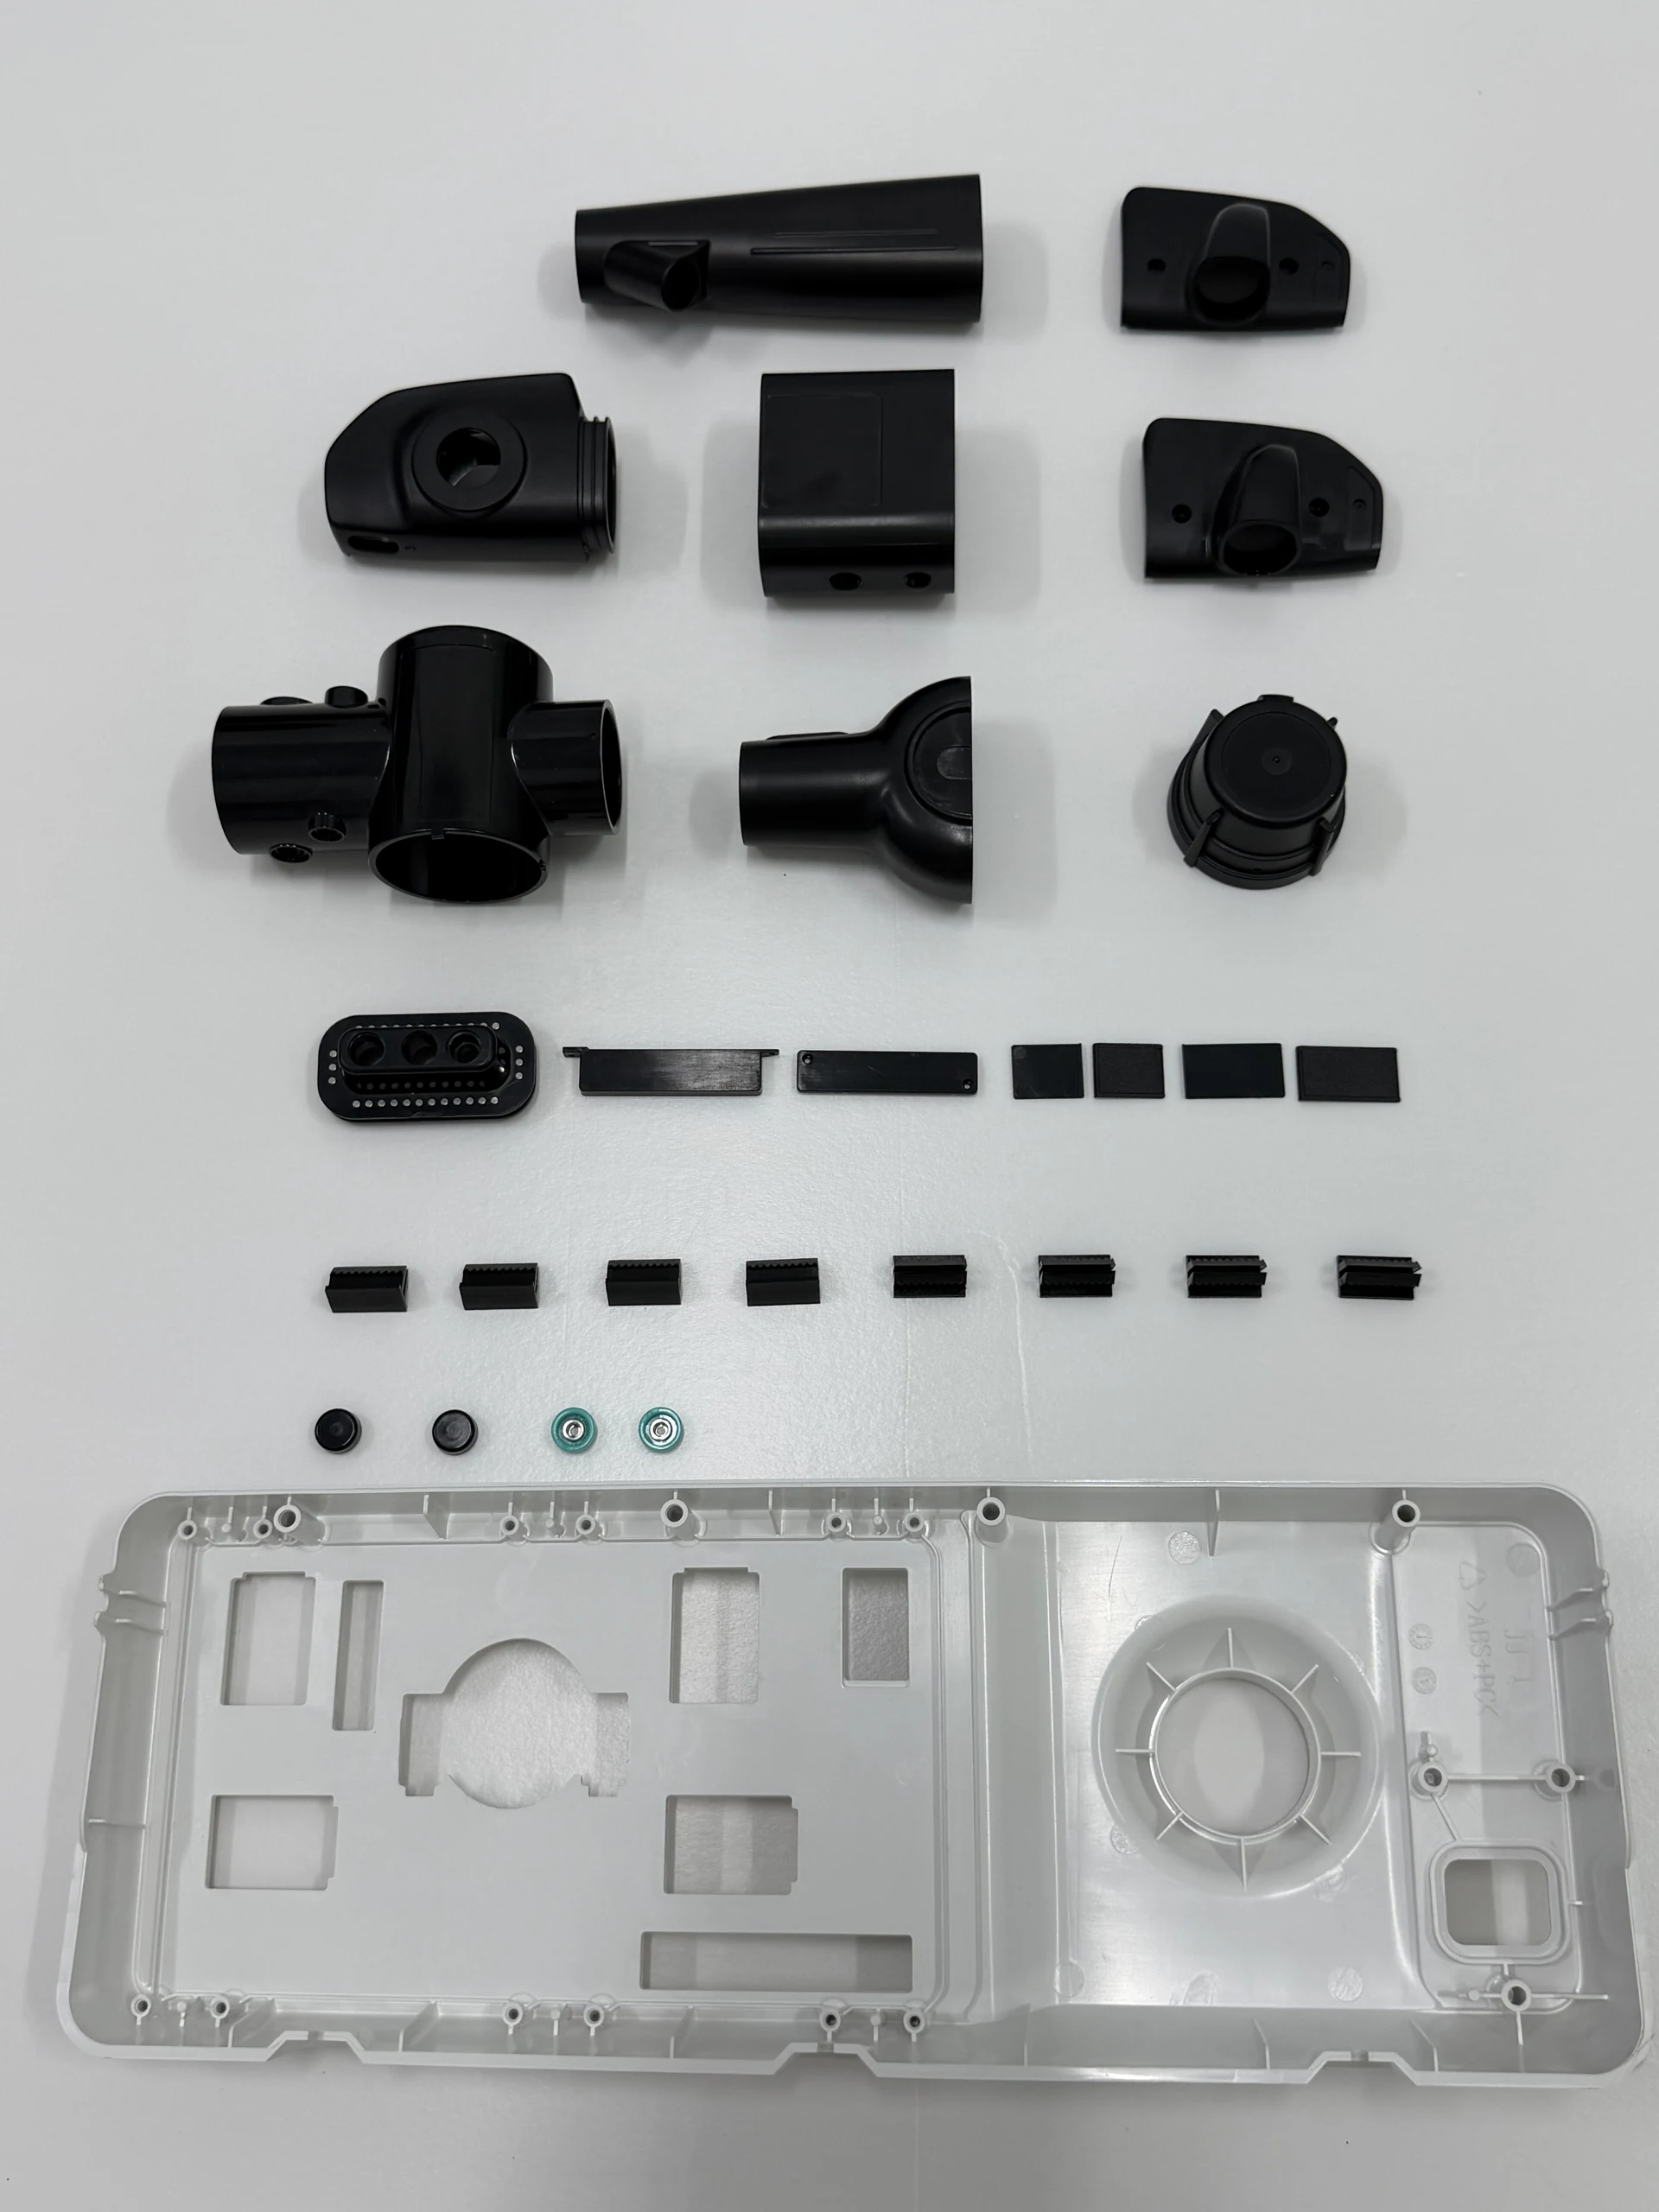
Equipment, lead time and order planning
Planning item
Basis for quotation
DFM review
Indicative 3–5 working days after complete drawings and requirements.
New tooling
Indicative 6–8 weeks to first tool trial after tool-design approval and commercial release; corrections and customer validation are additional.
Order quantities
Initial quotation-planning basis: a 500-piece pilot or 1,000-piece repeat batch per part number, resin and colour, subject to project quotation.
Repeat orders
Indicative 10–15 working days after materials and the production slot are confirmed. Customer qualification, special processing and transit are additional.
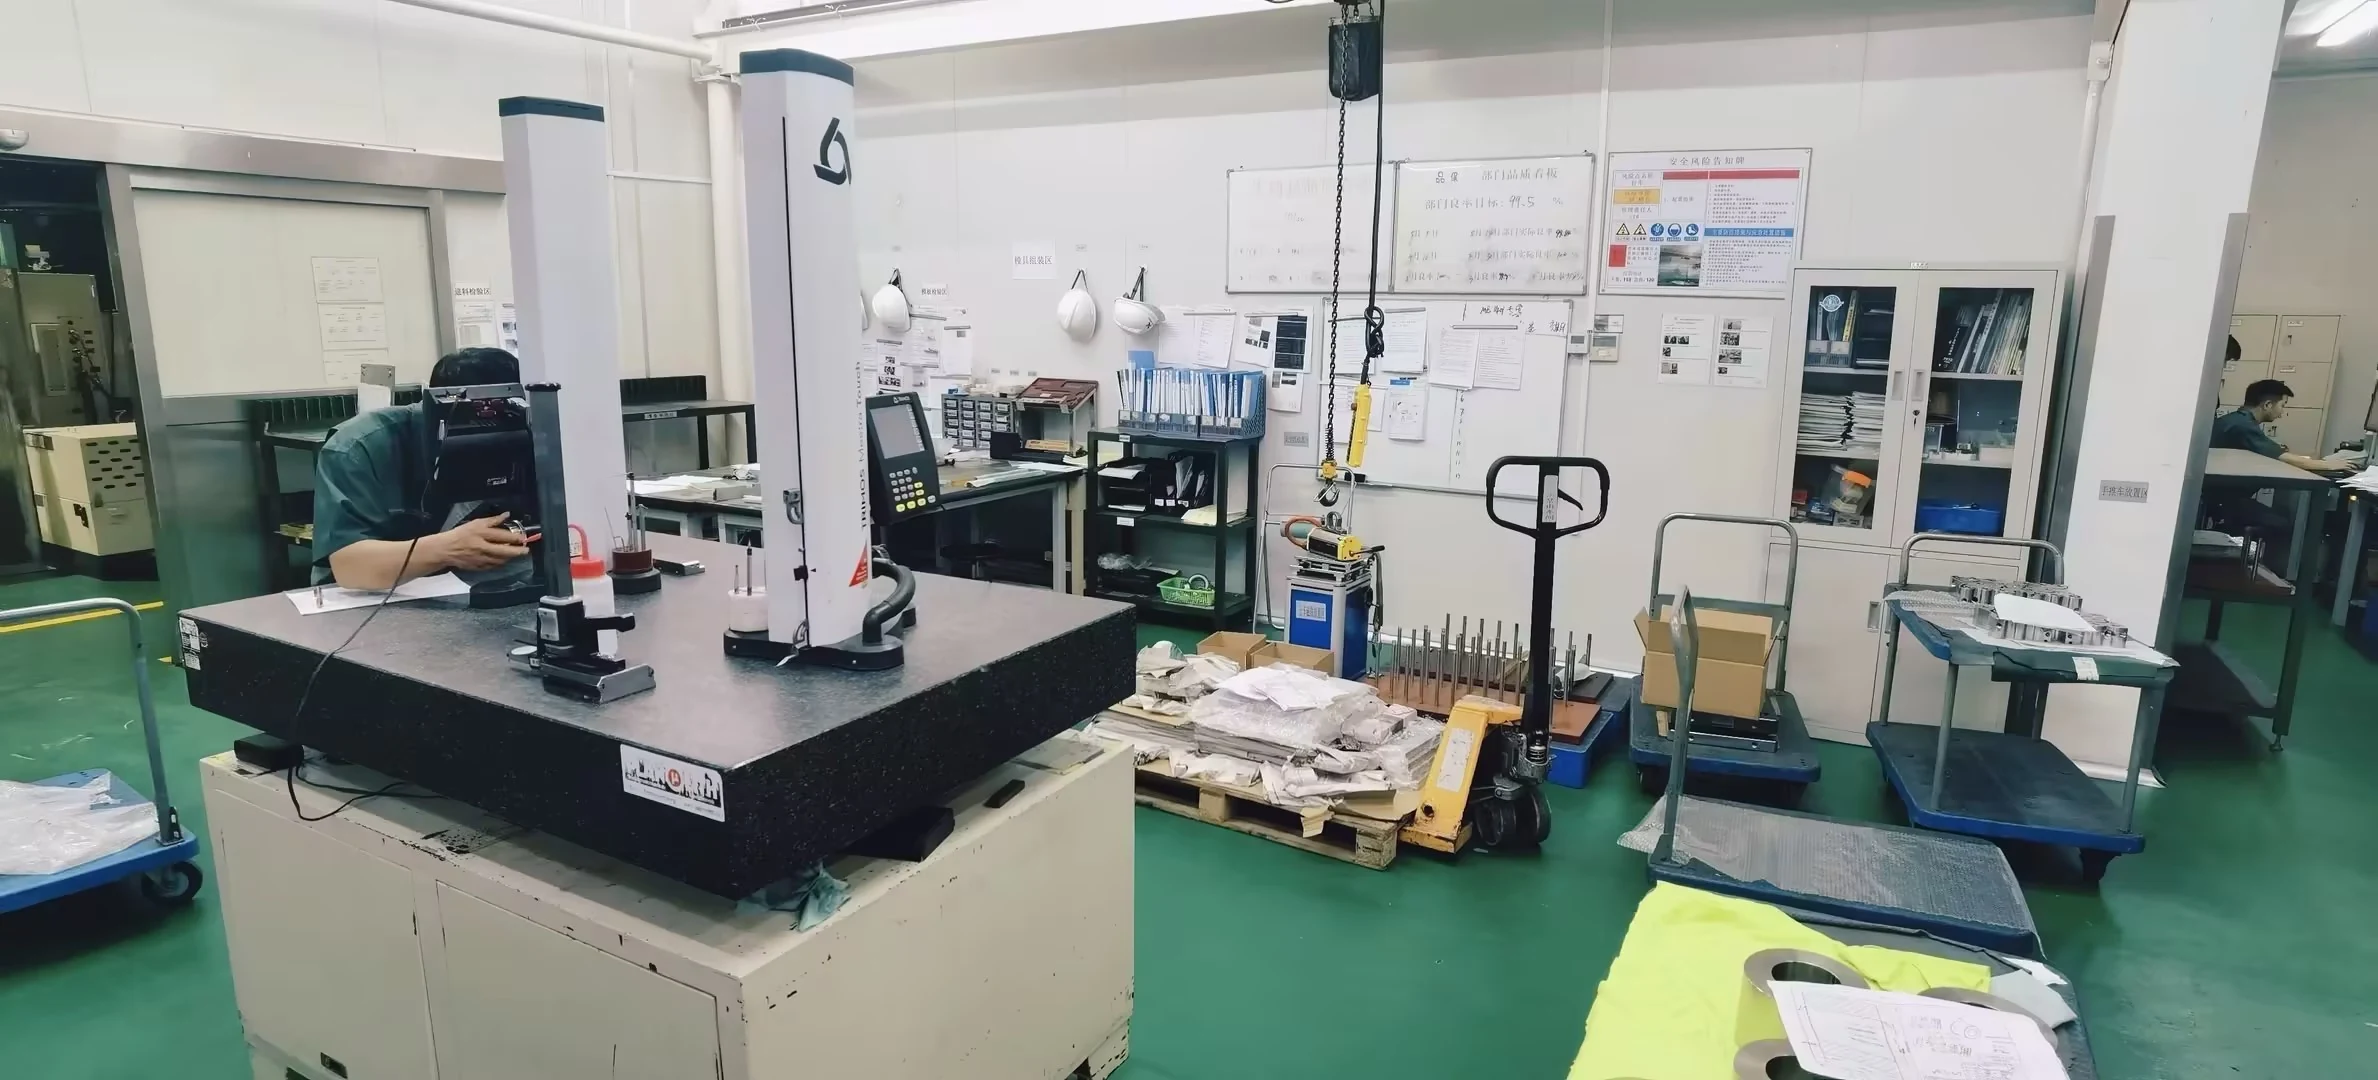
Keep repeat orders on an approved baseline
Where these components can be used
Technical Specifications
| Process | Custom precision plastic injection molding |
|---|---|
| Product Group | Endoscope Waterproof Connectors and Assembly Components |
| Typical Applications | multi-pin waterproof connectors, cable interfaces and coordinated endoscope subassemblies |
| Material Options | PC/ABS, ABS, PA, POM, TPE and other engineering resins selected for device assembly and cleaning requirements |
| Engineering Focus | accurate pin and connector alignment, stable sealing grooves and overmold interfaces, and protected cable routing through assembled components |
| Project Support | DFM review, mold design, mold trials, assembly validation and repeat production |
| Customization | Geometry, color, texture, resin, inserts and packaging can be developed to project requirements |
Recommended Products
Explore our high-precision injection moulded components trusted by industry leaders worldwide.