English
 Español
 Português
 Русский
 العربية
 Français
 Deutsch
 中文
 日本語
 한국어


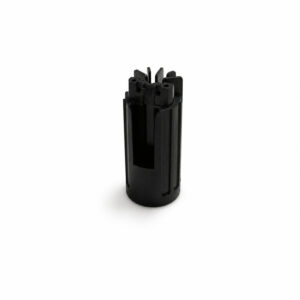
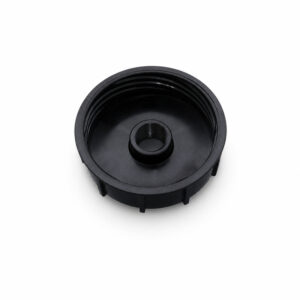
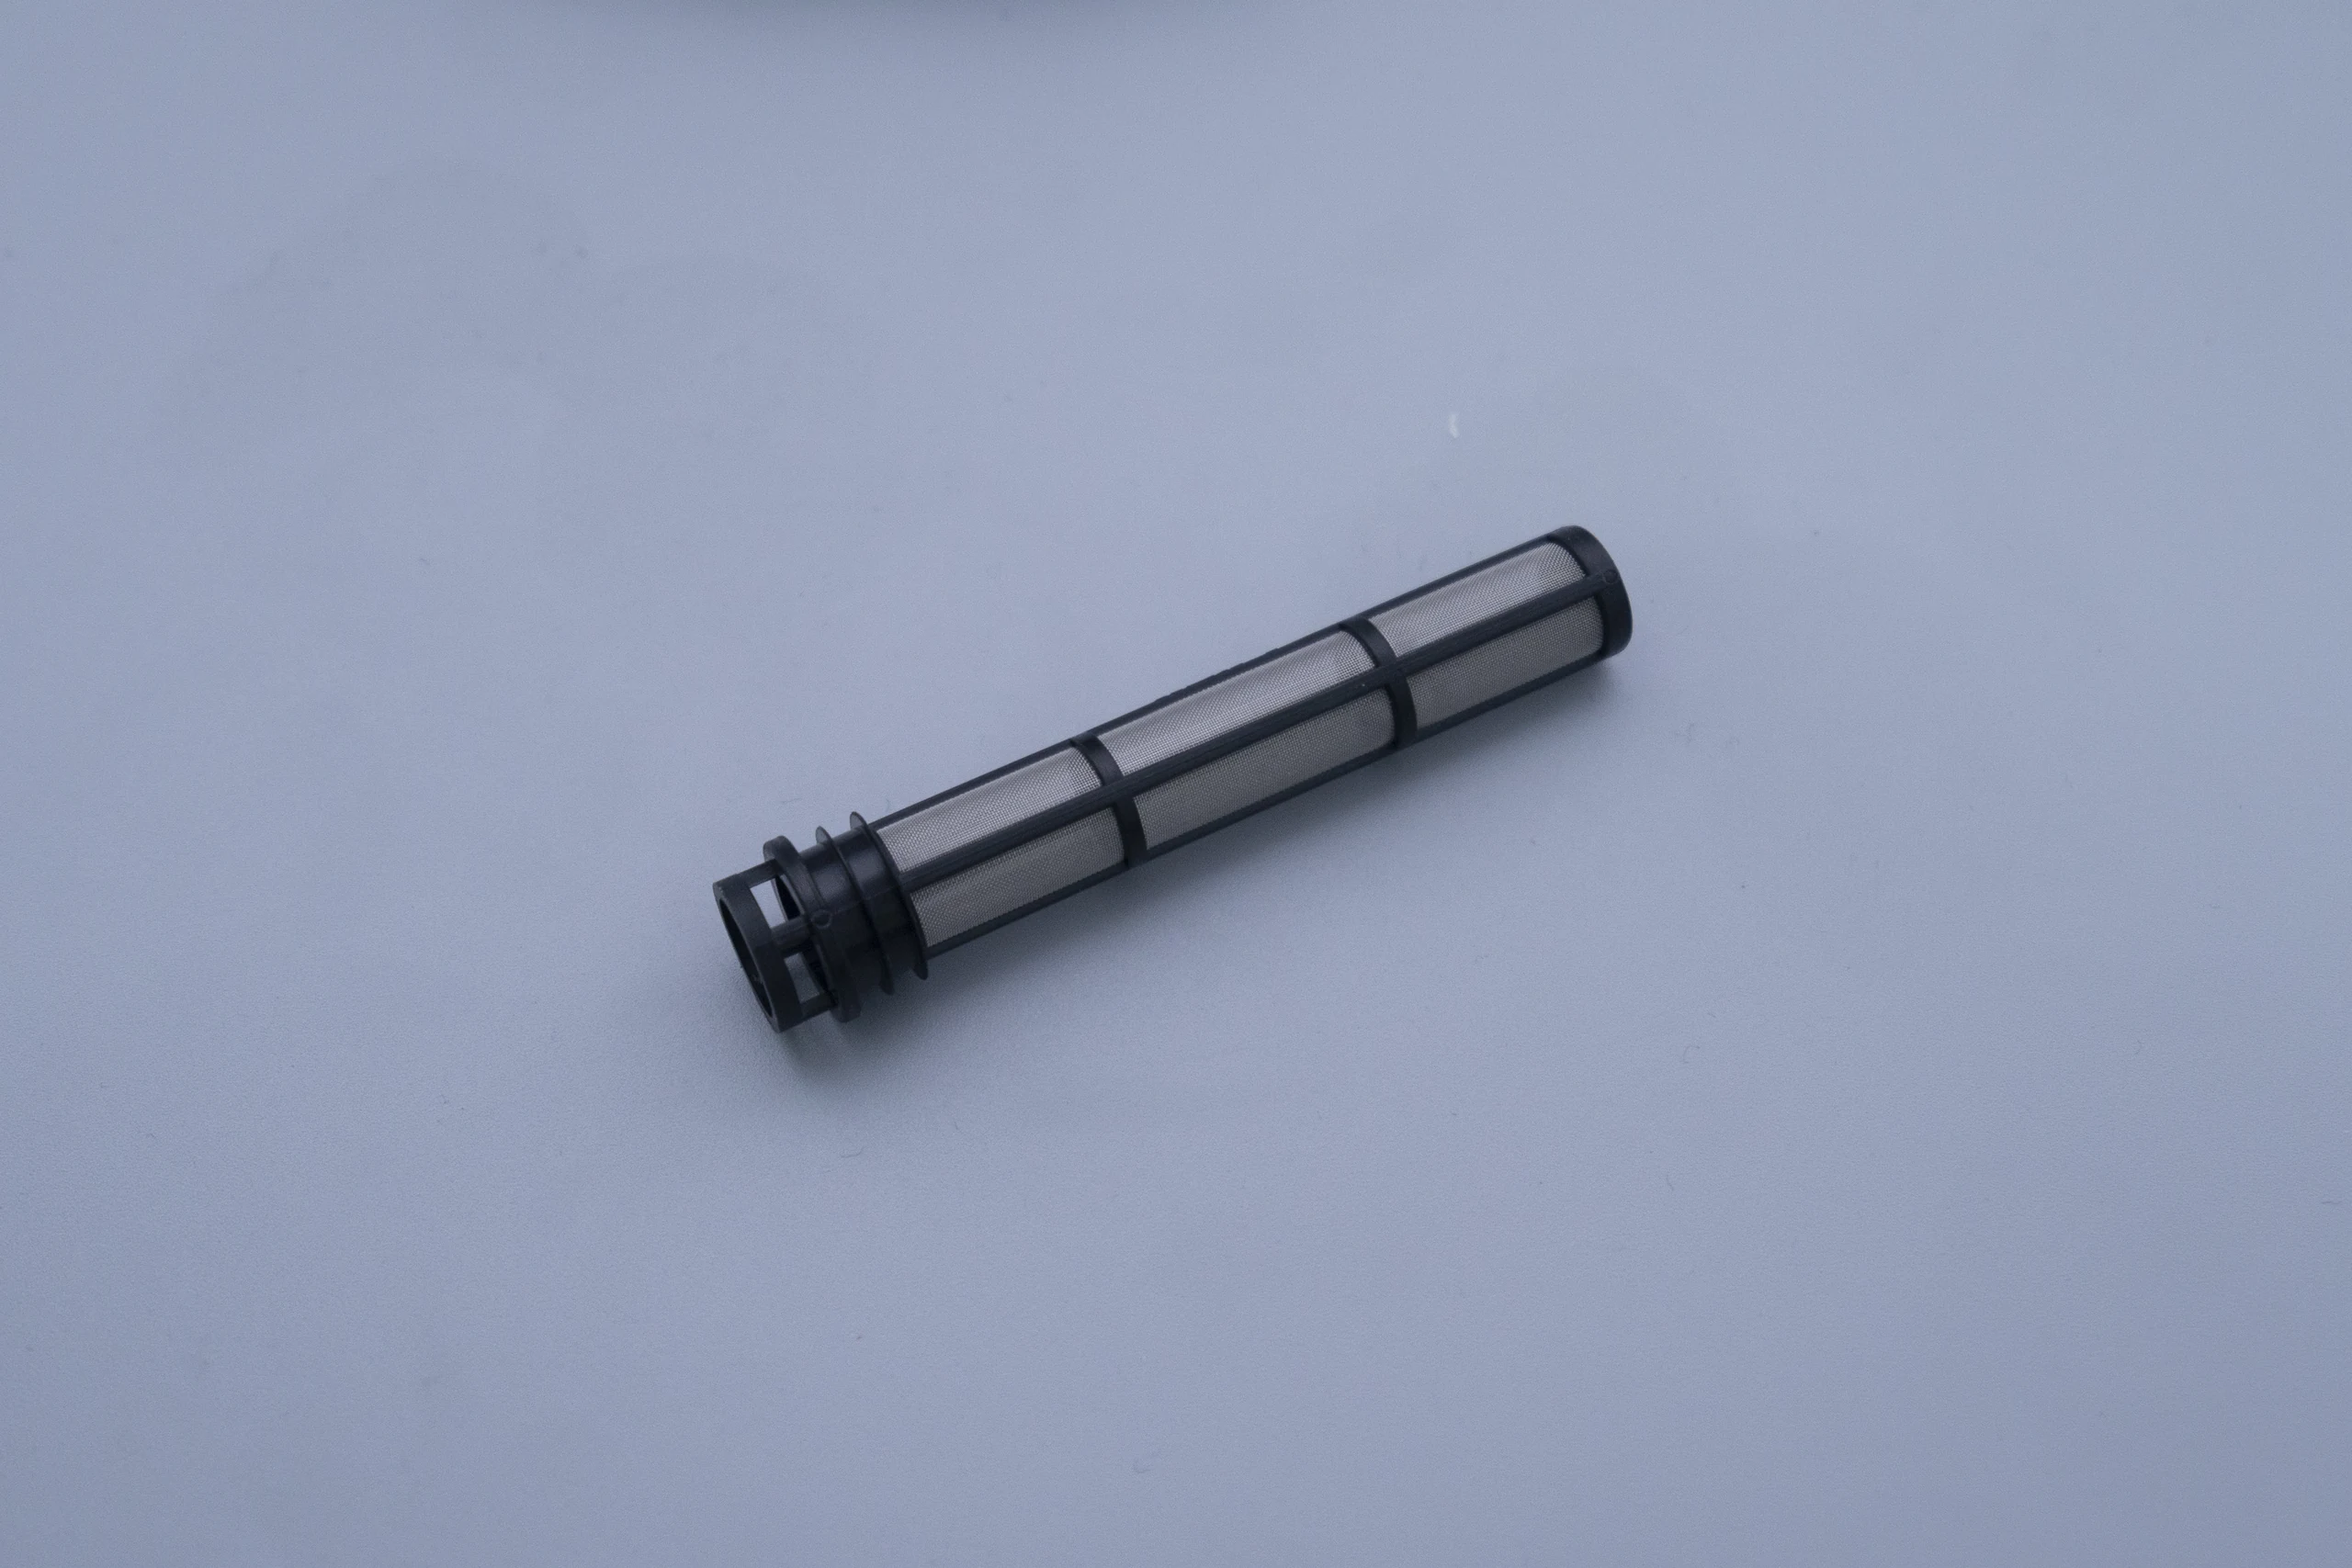
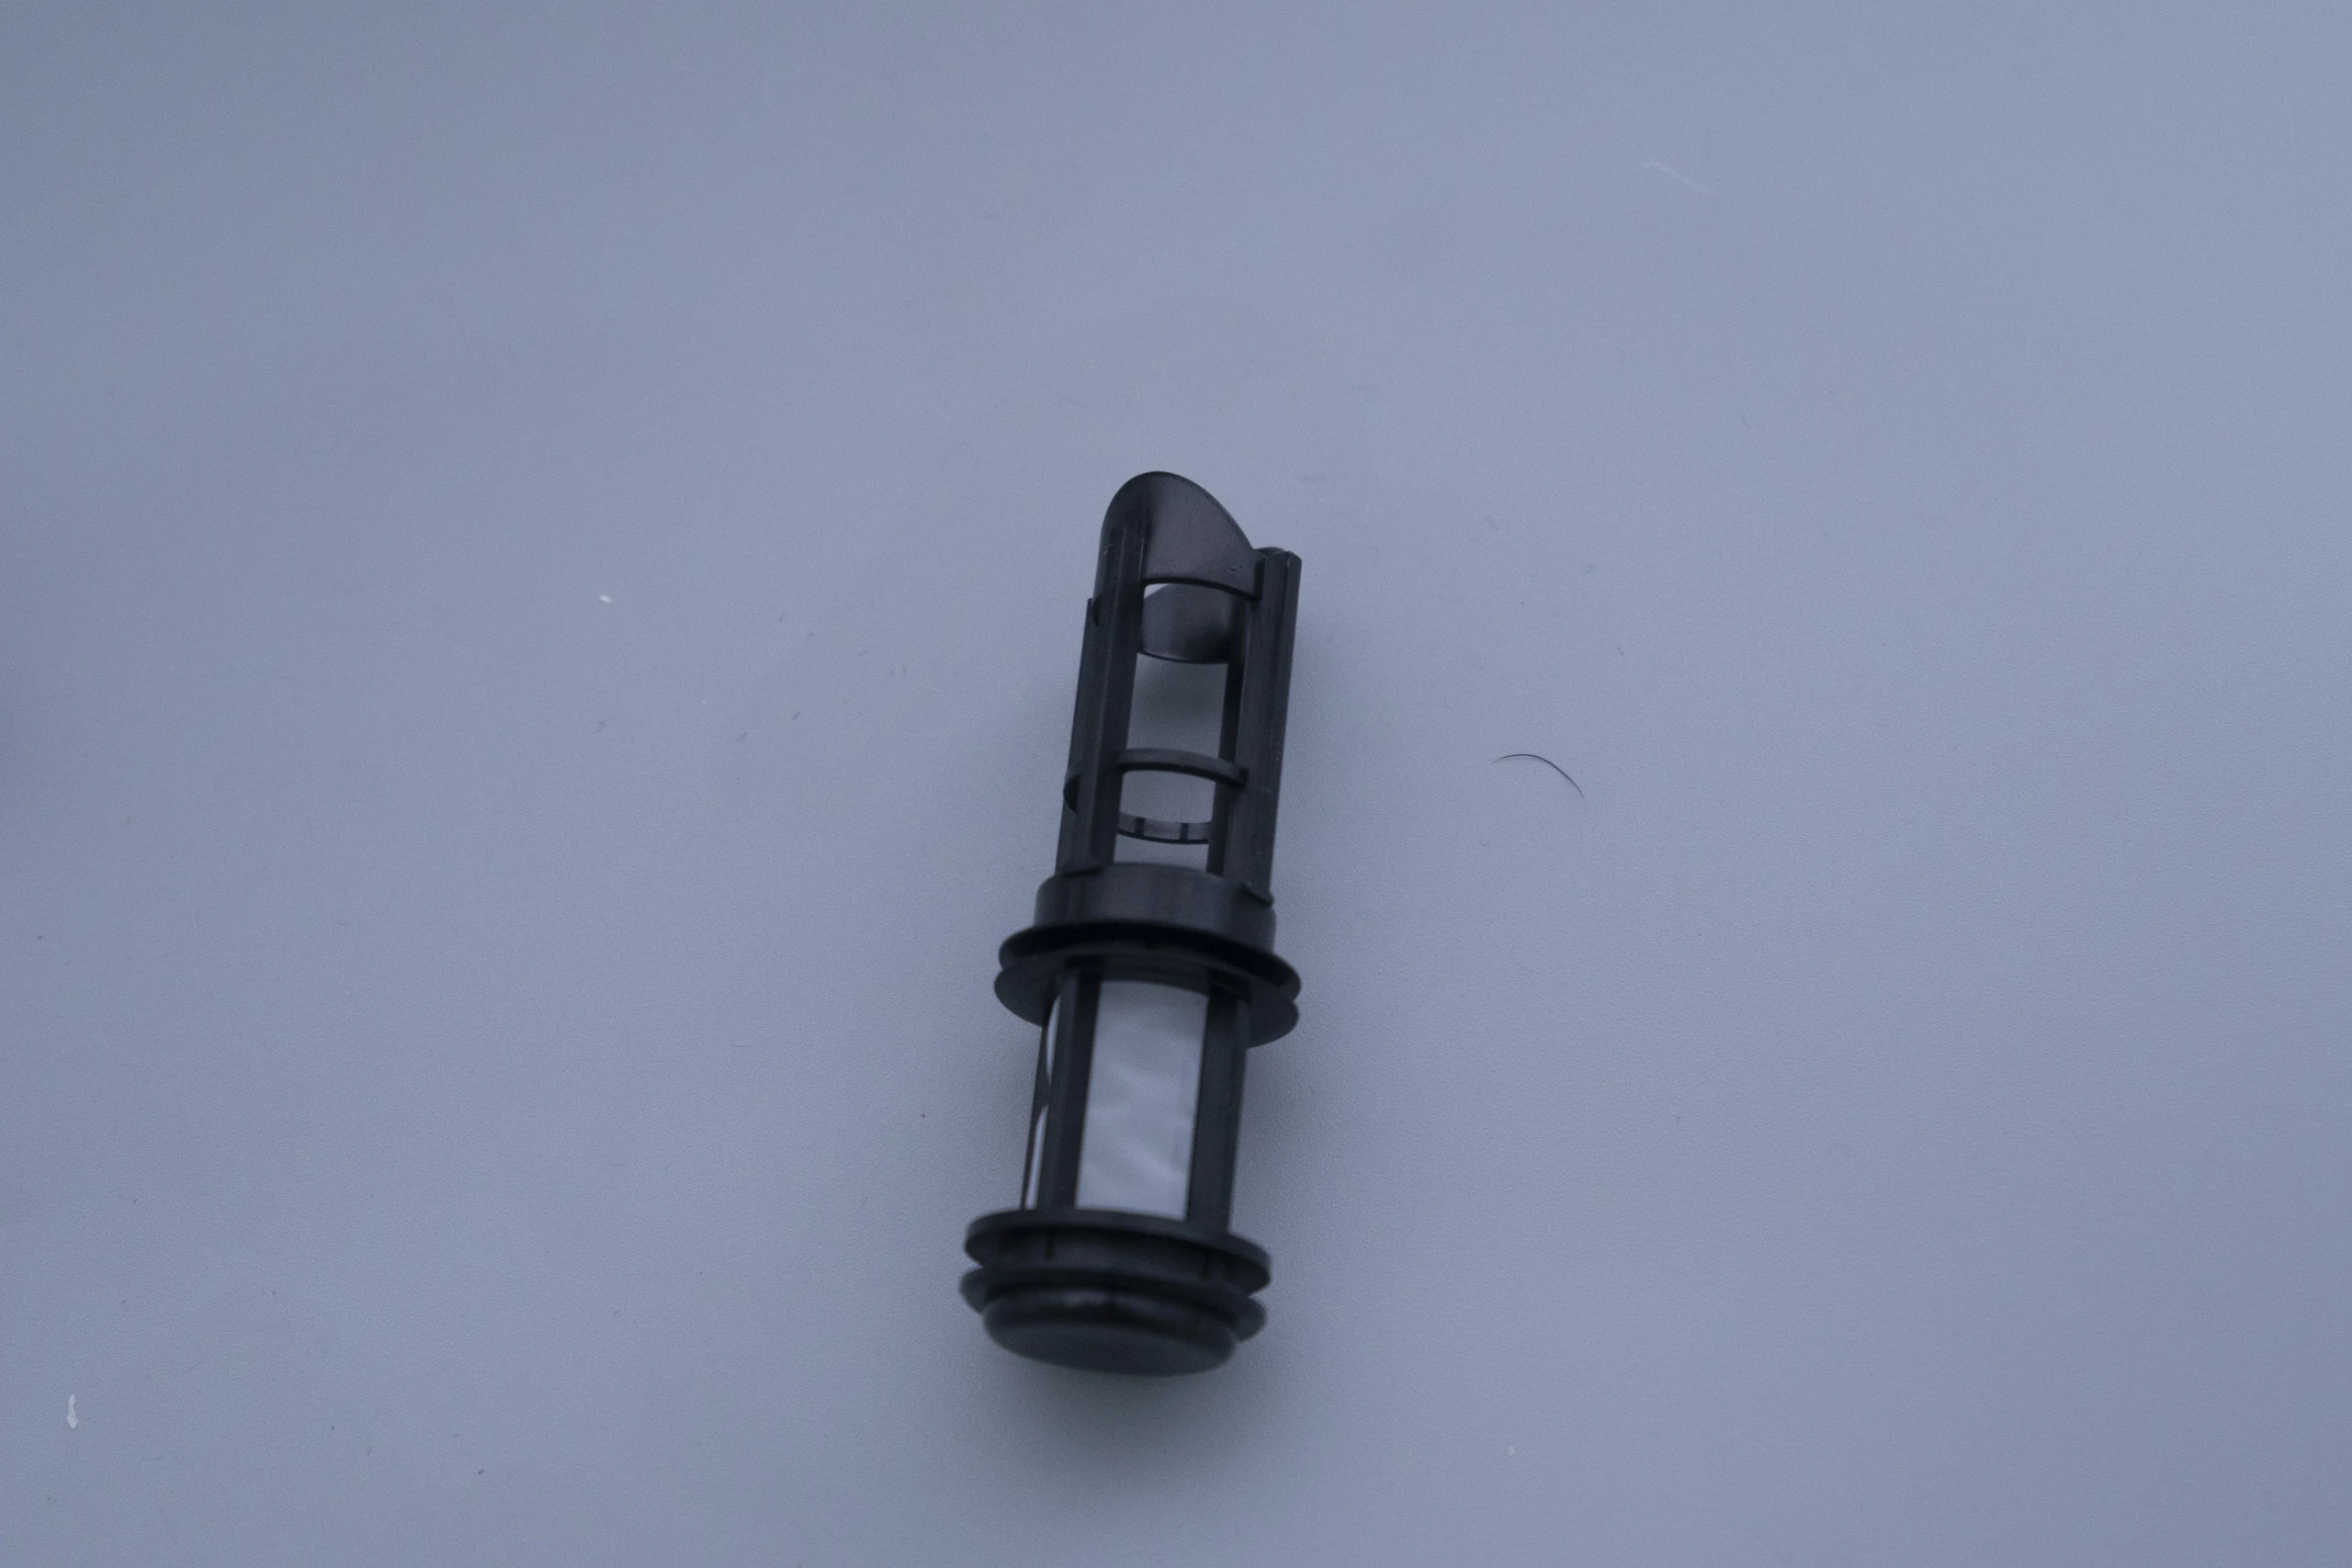
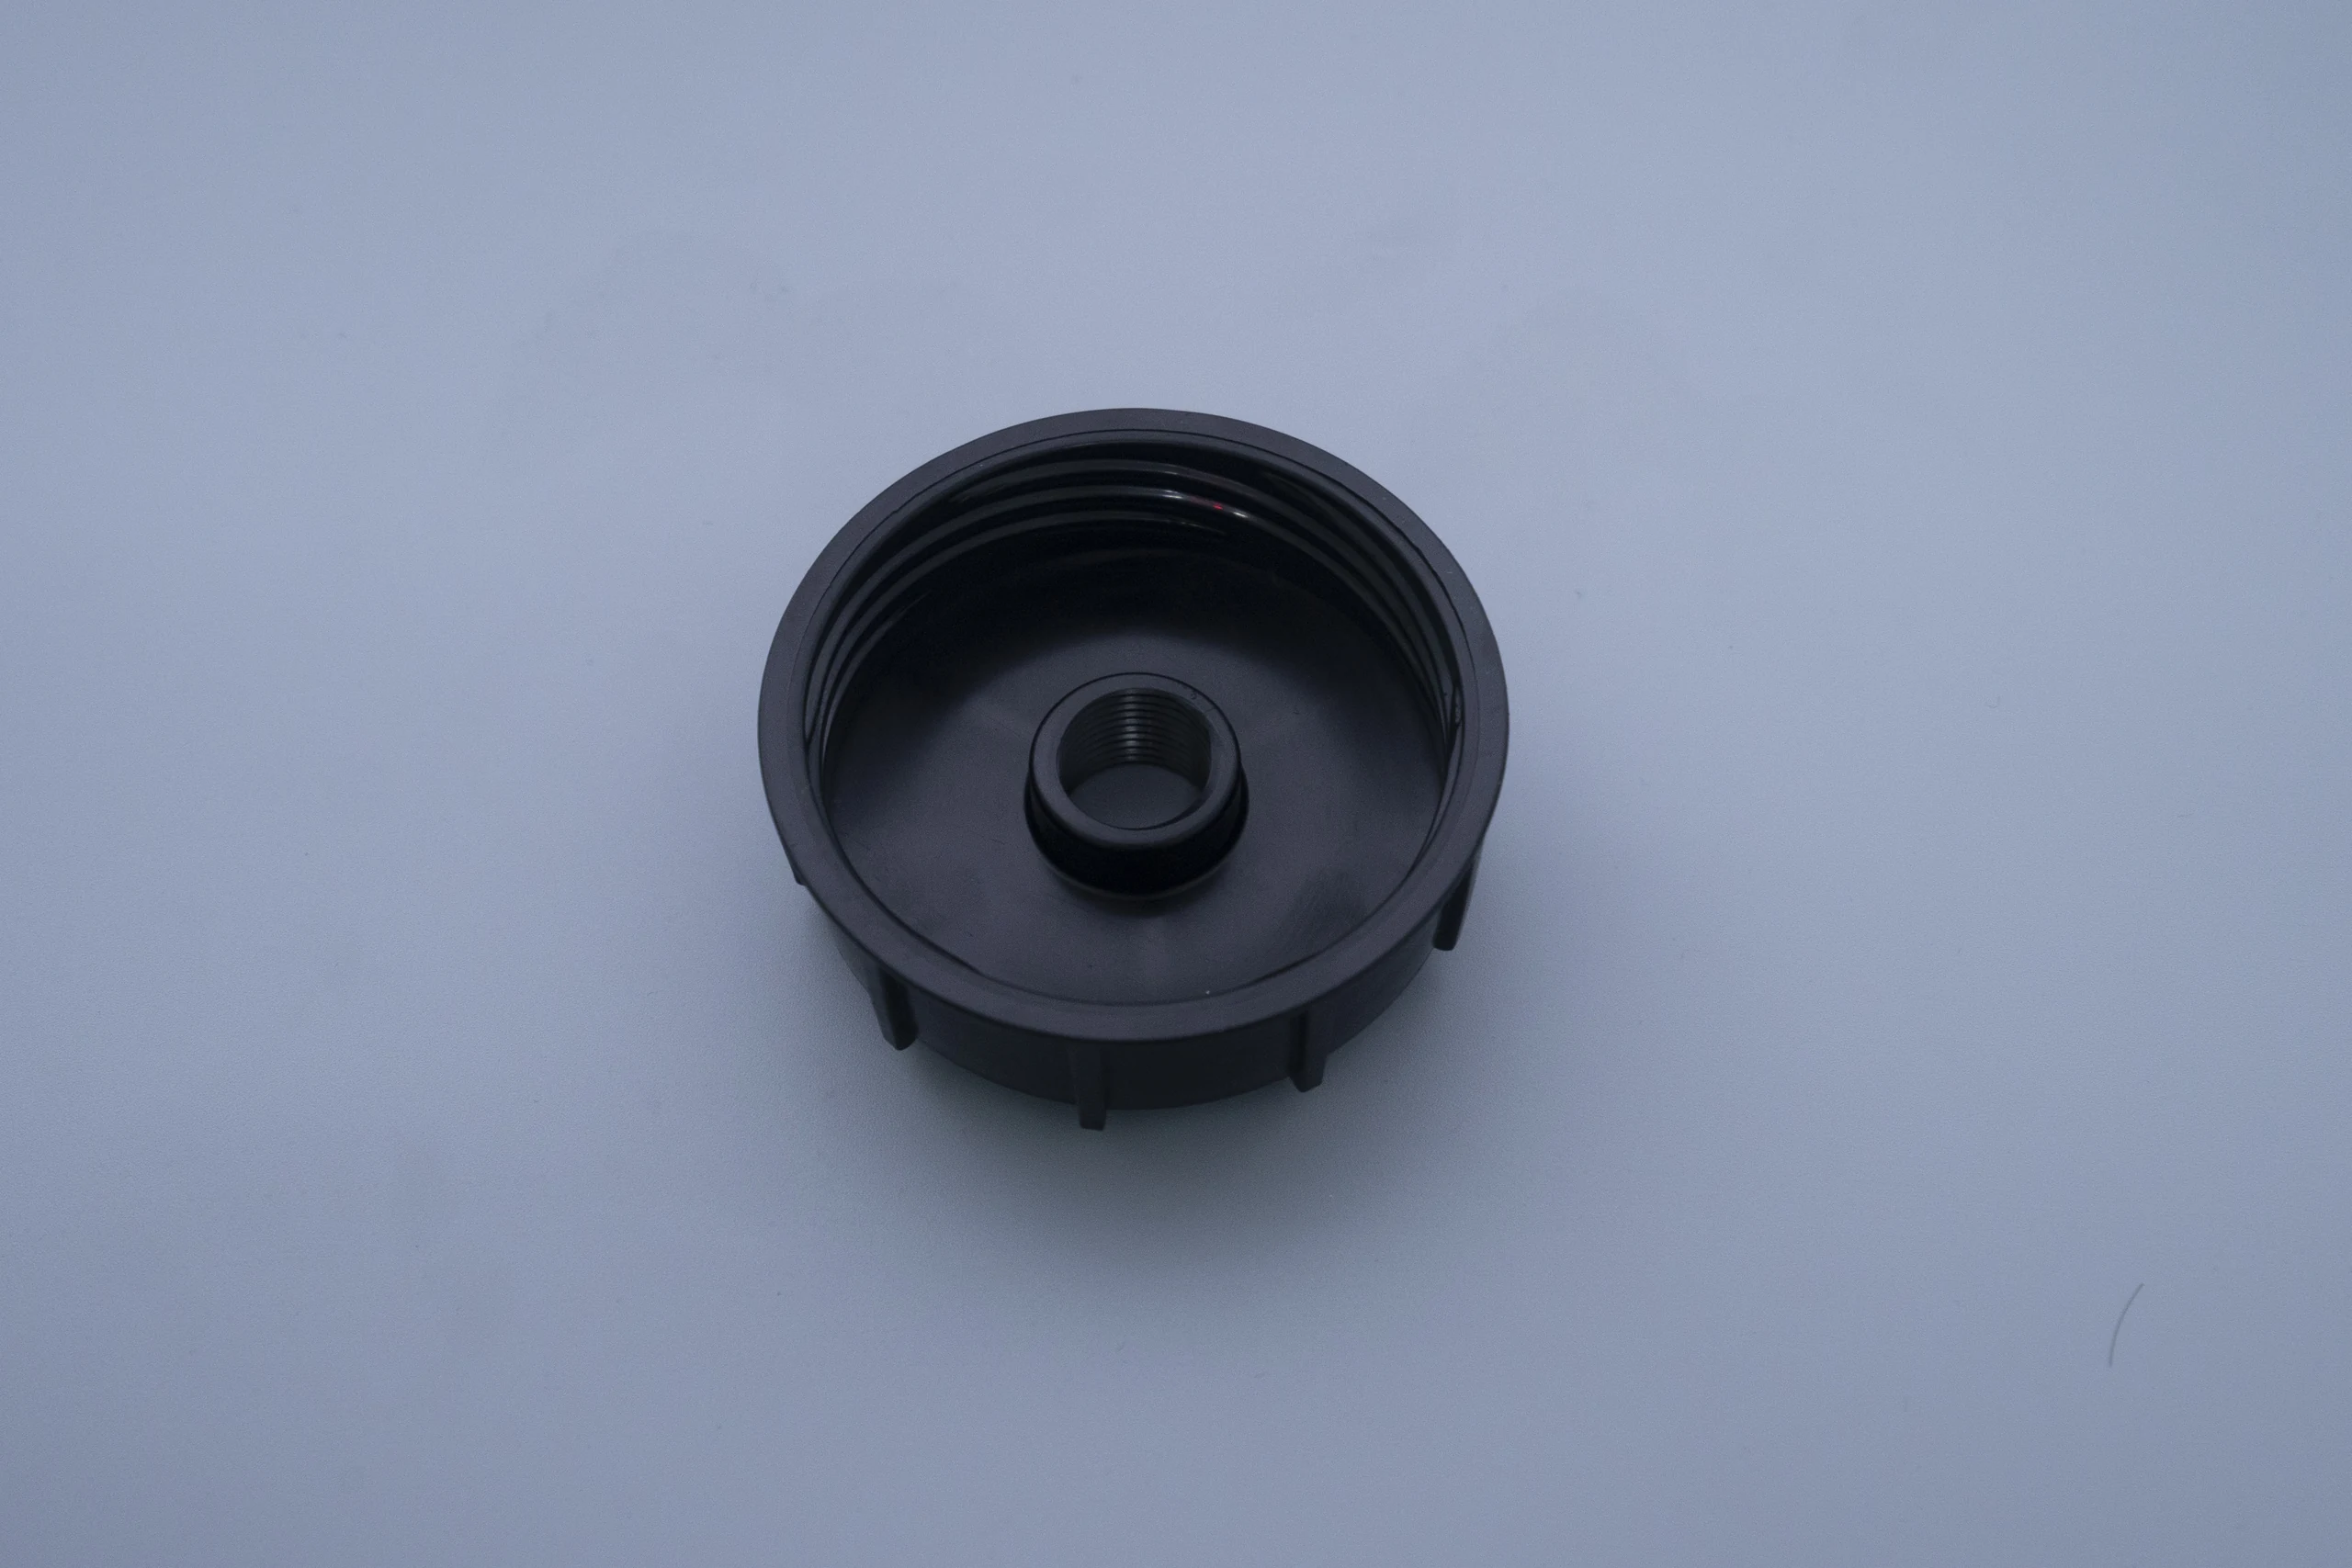
Long Filter Cores and Threaded End Caps
JingZhan develops custom long filter cores and threaded end caps for long filter cores, replaceable mesh elements and threaded cartridge closures. The molding plan is developed around straight cores over long molded lengths, clean, repeatable threaded end connections, and secure mesh retention and concentric cartridge assembly. Resin selection, gate location, parting lines and inspection points are matched to the mating parts, operating environment and expected production volume.
Product Overview
JingZhan develops custom moulded long filter supports, tubular cores and end caps for customer-designed assemblies. The manufacturing review connects the core's straightness and support features with the mating thread, rim and housing. The quoted scope follows the approved component drawing; filter media and finished-cartridge performance are separately defined. DESIGN AND MANUFACTURING Identify the support points and features that locate the core in its intended housing. Review slender sections, wall transitions and core support during tool design, and agree how straightness or distortion will be checked. Provide the mating thread or engagement drawing, including relevant datums and end faces. Review the parting line and demoulding route, then confirm the fit using agreed gauges or representative mating parts. Identify any gasket contact, sealing rim, stop face or retention feature. Define the assembly and test requirements together; the presence of a thread does not itself establish a leak-tight or pressure-rated joint. Confirm the fluid, temperature, loading and cleaning conditions. Review the resin grade, stiffness and dimensional behaviour against that scope, along with permitted gate, flash and ejector marks on functional areas. TECHNICAL SPECIFICATIONS PRODUCTION AND REPEAT SUPPLY The proposed route uses CNC/EDM mouldmaking and injection moulding with a tool arrangement suited to the long core and end features. JingZhan's listed machining, EDM, moulding and dimensional/vision inspection resources provide project-specific options. Press allocation follows the actual tool envelope, projected area, shot volume and selected resin. Approve the resin, drawing revision, thread-fit sample and inspection fixtures before repeat production. Define startup checks for core alignment, engagement and end faces. Review maintenance affecting long cores or threaded inserts before the next batch is released against the approved baseline. Tooling investment is quoted separately from the piece price. Share annual demand and release quantities so cavity count, procurement and batch cost can be reviewed together. RELATED APPLICATIONS Long support cores and end components for custom fluid-filtration cartridges. Threaded closures and locating parts coordinated with customer-designed filter housings. Related tubular or end-cap components used in industrial fluid-system development and assembly projects. A plastic core or threaded cap does not establish filtration performance or a universal working-pressure rating. Flow, medium compatibility, sealing performance and durability are specified and qualified for the complete customer assembly and agreed conditions. Discuss your drawing and supply requirements. Send CAD, resin preference, critical features, annual demand and release quantity. Contact our engineering team →Long filter supports and end caps with controlled mating geometry
Key processing requirements
Control the long core as a functional part
Define the thread and engagement
Coordinate sealing and retention
Choose the grade for actual exposure
Parameters agreed for your part
Parameter
Project specification
Component range
Long filter supports, tubular cores, threaded end caps and related moulded end parts.
Material selection
PP, PA, PBT, POM or another approved resin and grade reviewed for the application.
Length and section
Custom to approved drawings, with slender-core and wall-balance DFM review.
Thread or engagement
Customer-defined profile, mating data, engagement depth and checking method.
Sealing interfaces
Specified rim, gasket contact and end-face requirements for the intended assembly.
Critical inspection
Drawing-defined dimensions, fit, straightness and agreed visual limits.
Tool configuration
Core support, cavity count and demoulding approach selected for geometry and demand.
Delivery condition
Protected packing, component identification and scoped material/inspection records.
Equipment, lead time and order planning
Planning item
Basis for quotation
DFM review
Indicative 3–5 working days after complete drawings and requirements.
New tooling
Indicative 6–8 weeks to first mould trial after tool-design approval and commercial release; corrections and customer validation are additional.
Order quantities
Initial quotation-planning basis: a 500-piece pilot or 1,000-piece repeat batch per part number, resin and colour, subject to project quotation.
Repeat orders
Indicative 10–15 working days after materials and the production slot are confirmed. Customer qualification, special processing and transit are additional.
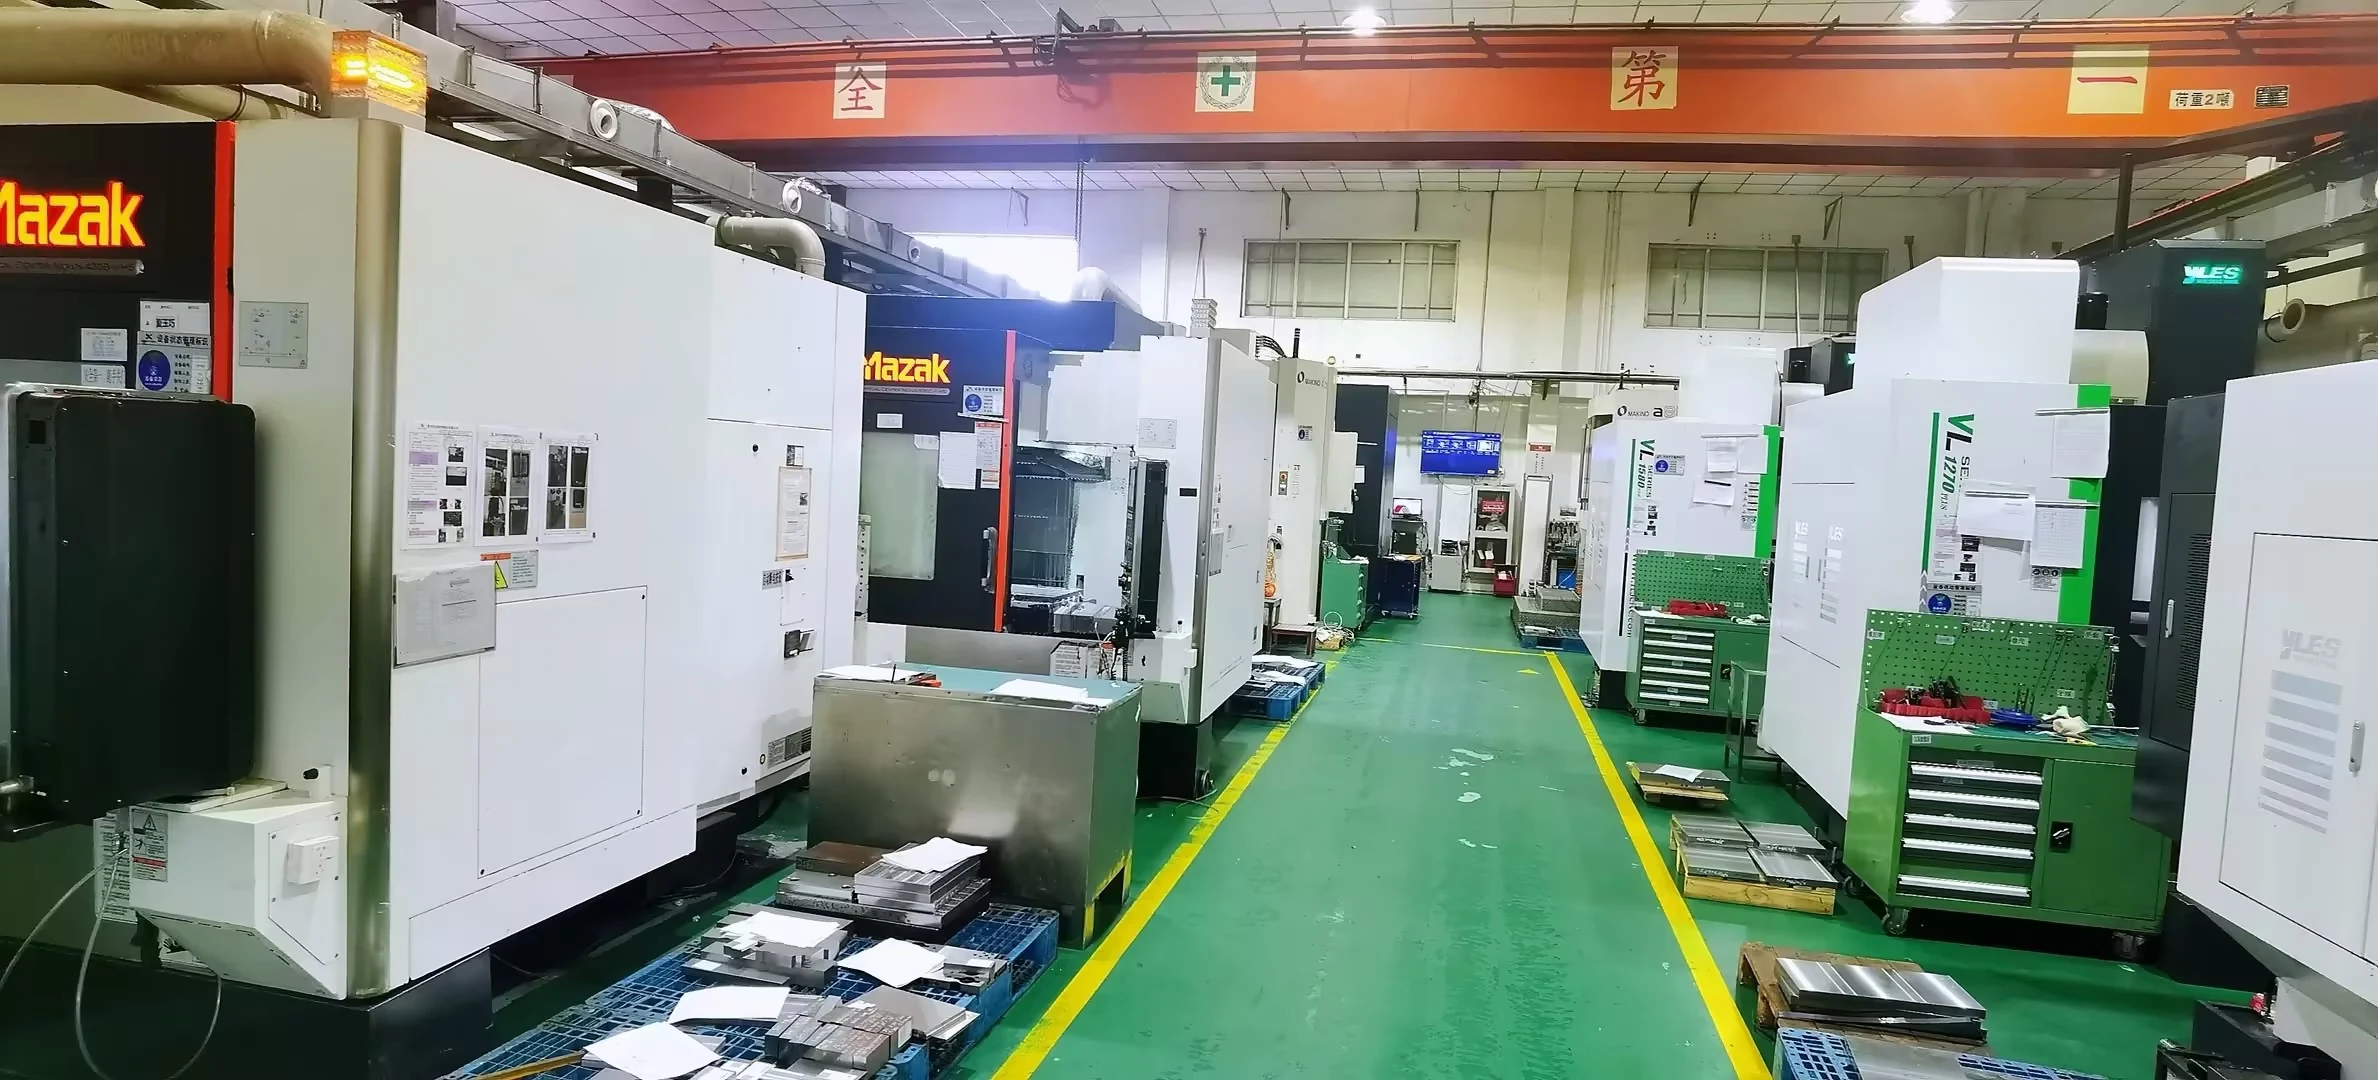
Keep repeat orders on an approved baseline
Where these components can be used
Technical Specifications
| Process | Custom precision plastic injection molding |
|---|---|
| Product Group | Long Filter Cores and Threaded End Caps |
| Typical Applications | long filter cores, replaceable mesh elements and threaded cartridge closures |
| Material Options | PP, PA, PBT, ABS and other chemical-resistant engineering resins selected for the fluid, temperature and pressure range |
| Engineering Focus | straight cores over long molded lengths, clean, repeatable threaded end connections, and secure mesh retention and concentric cartridge assembly |
| Project Support | DFM review, mold design, mold trials, assembly validation and repeat production |
| Customization | Geometry, color, texture, resin, inserts and packaging can be developed to project requirements |
Recommended Products
Explore our high-precision injection moulded components trusted by industry leaders worldwide.