 English
 Español
 Português
 Русский
 العربية
 Français
 Deutsch
 中文
 日本語
 한국어


Precision Injection Molded Parts
High-precision injection molded components manufactured with tight tolerances and premium-grade materials. Ideal for automotive, medical, electronics, packaging, and industrial applications. Custom mold design, rapid prototyping, and volume production available.
Product Overview
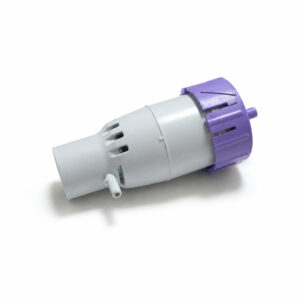
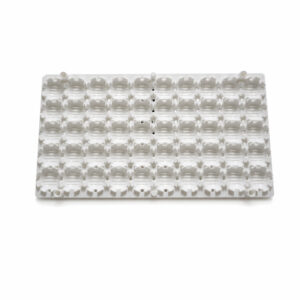
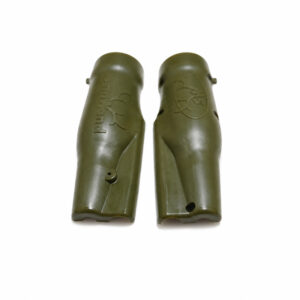
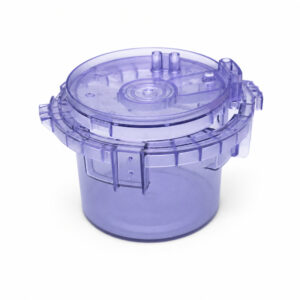
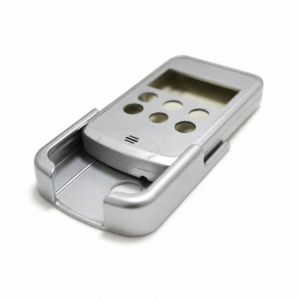
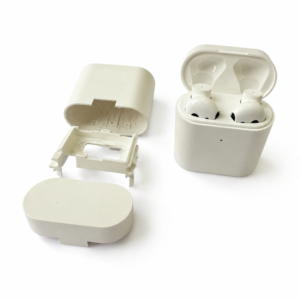
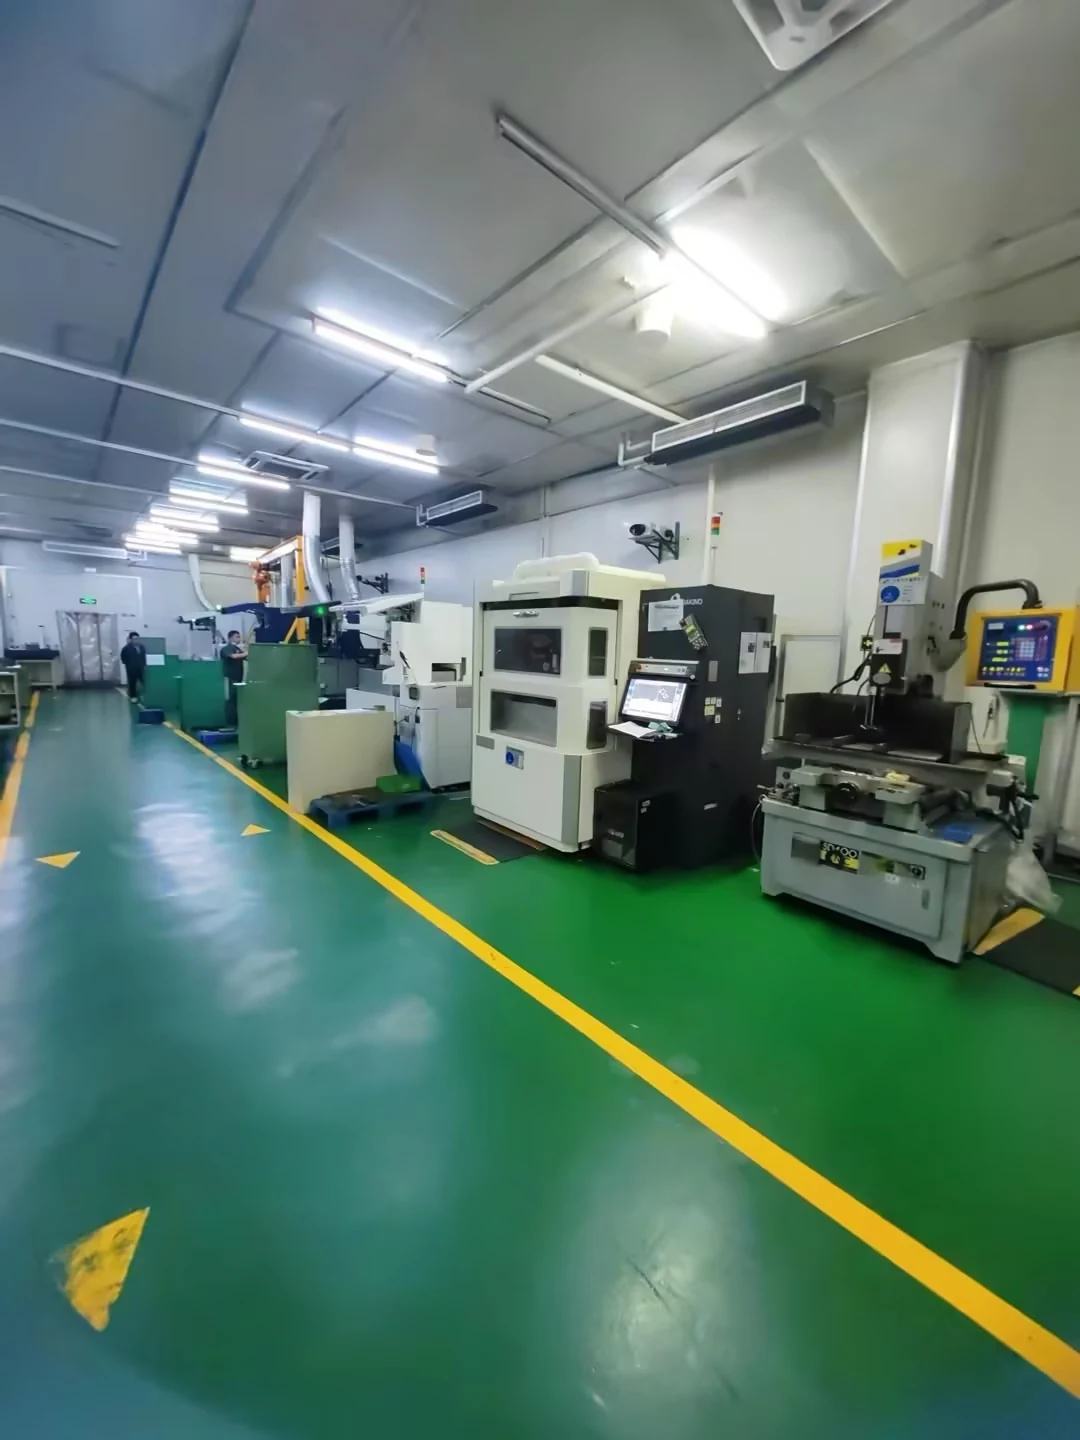
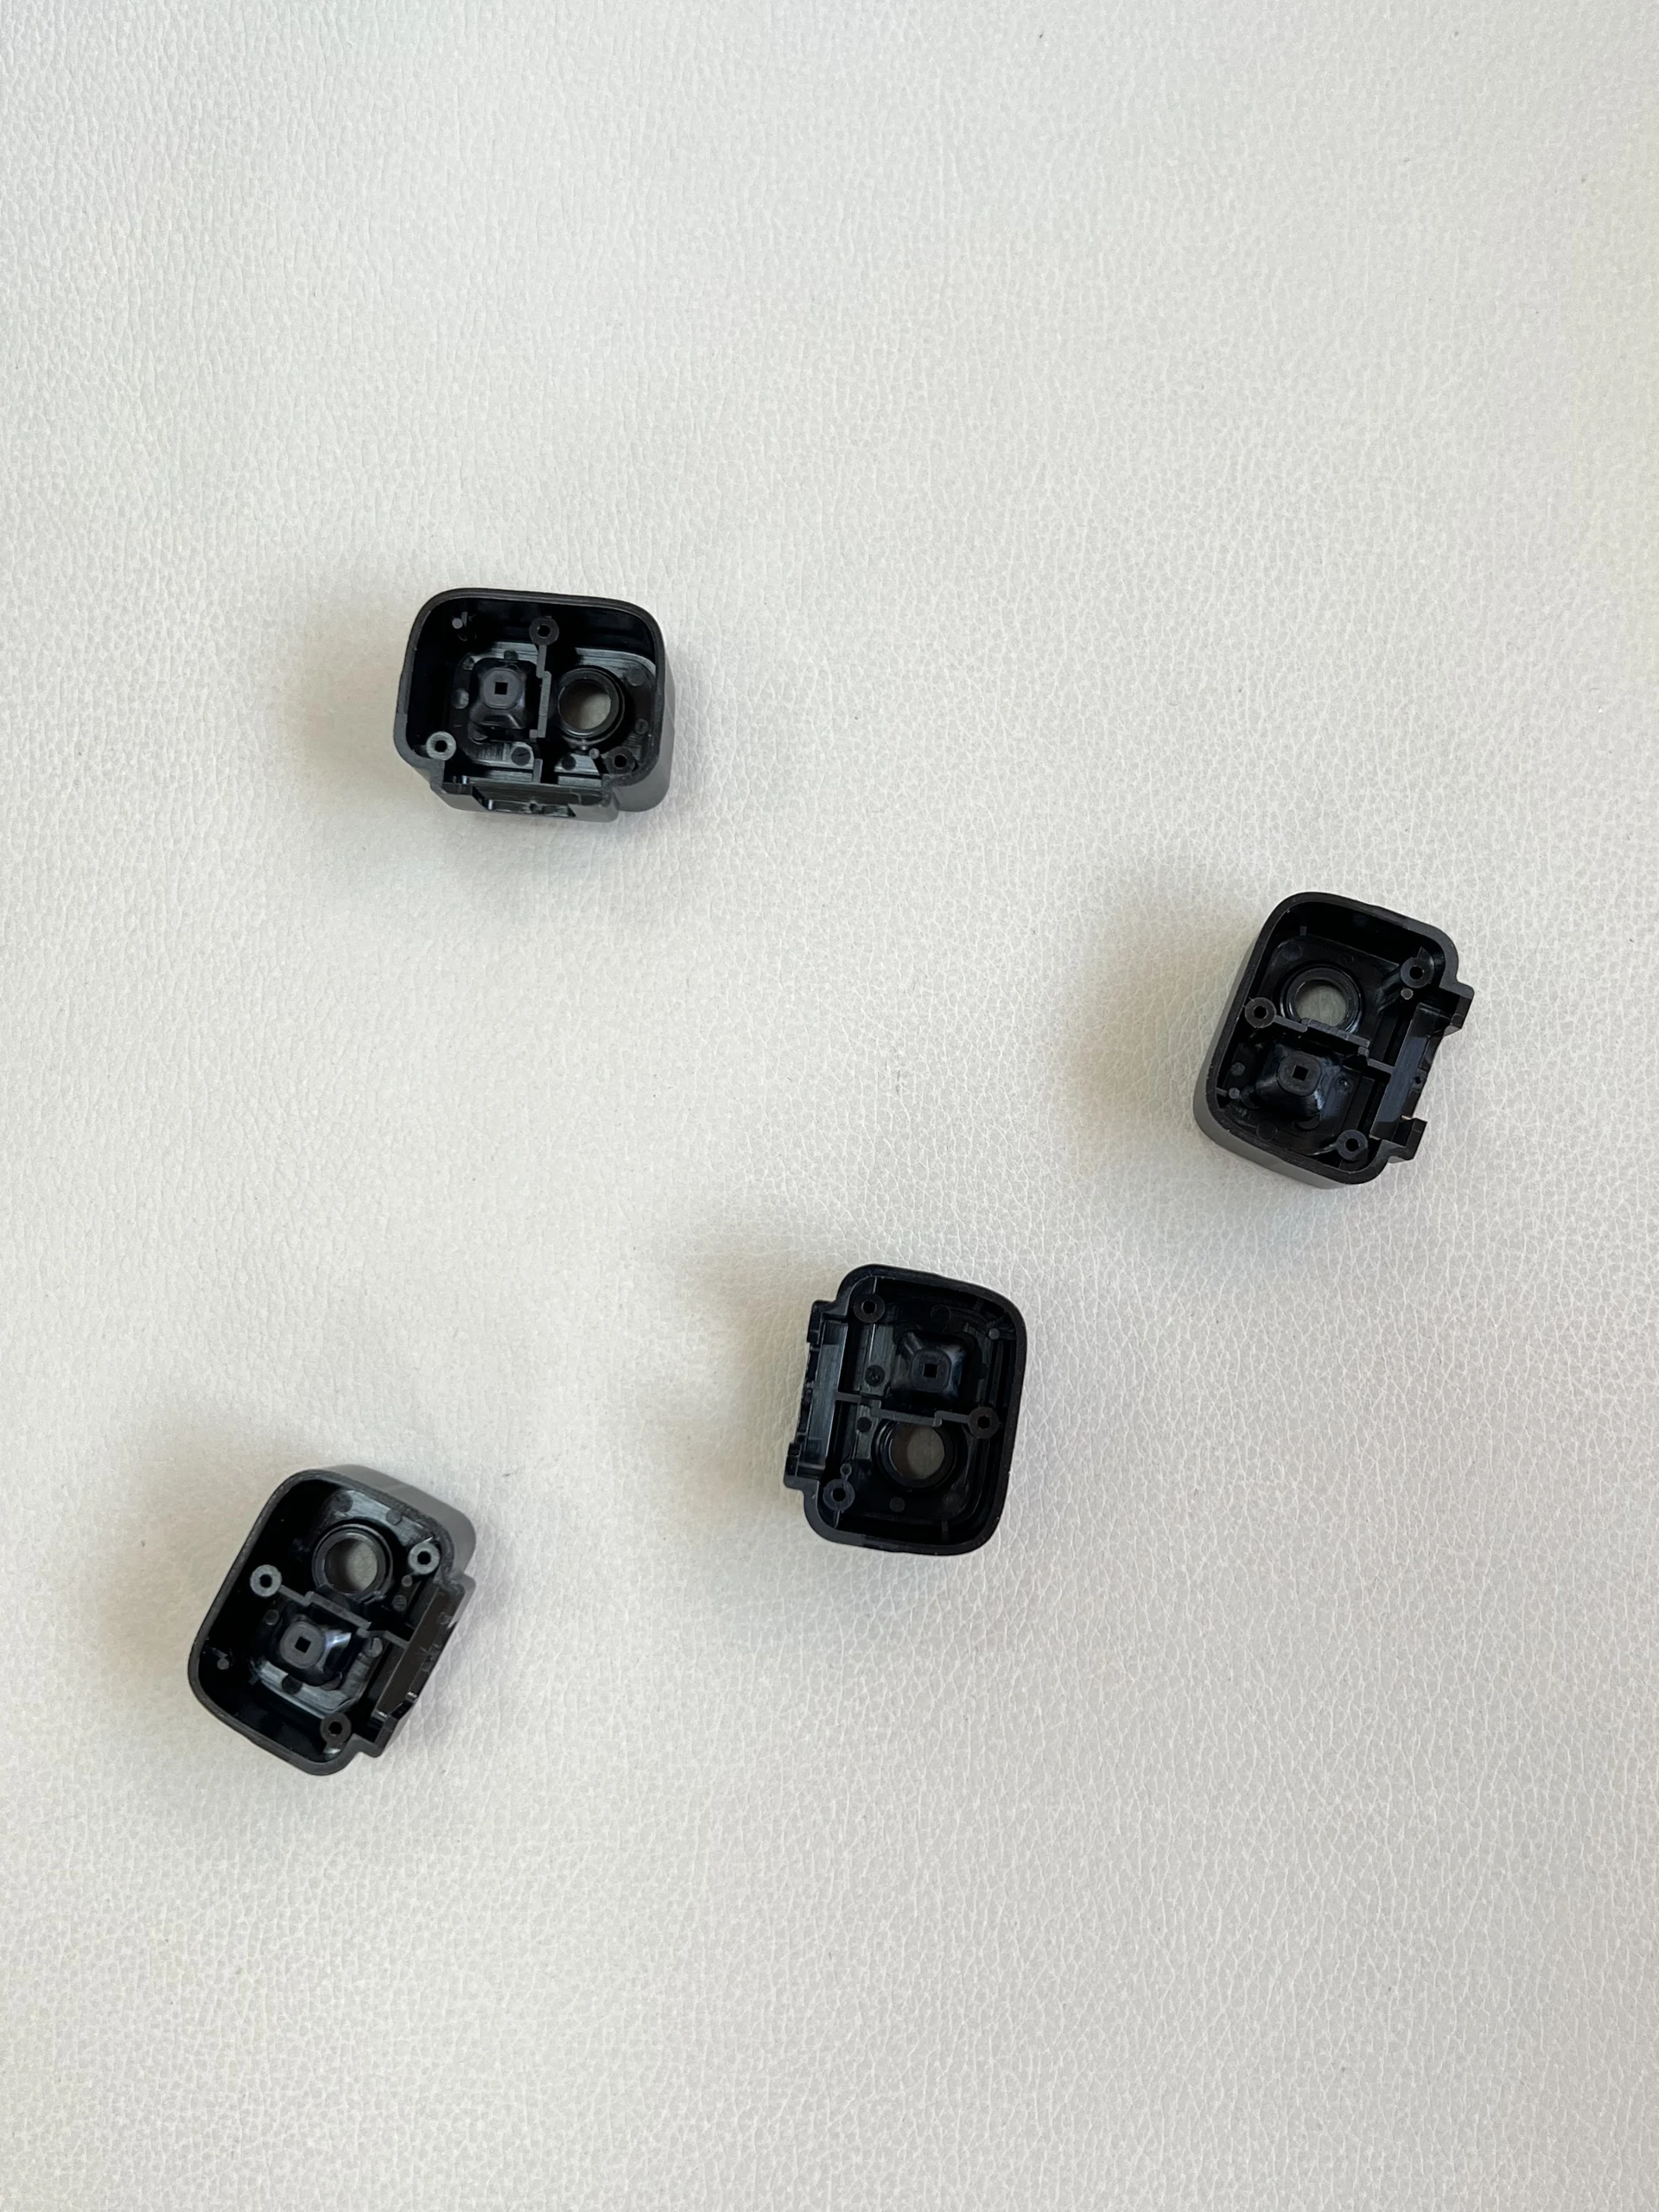
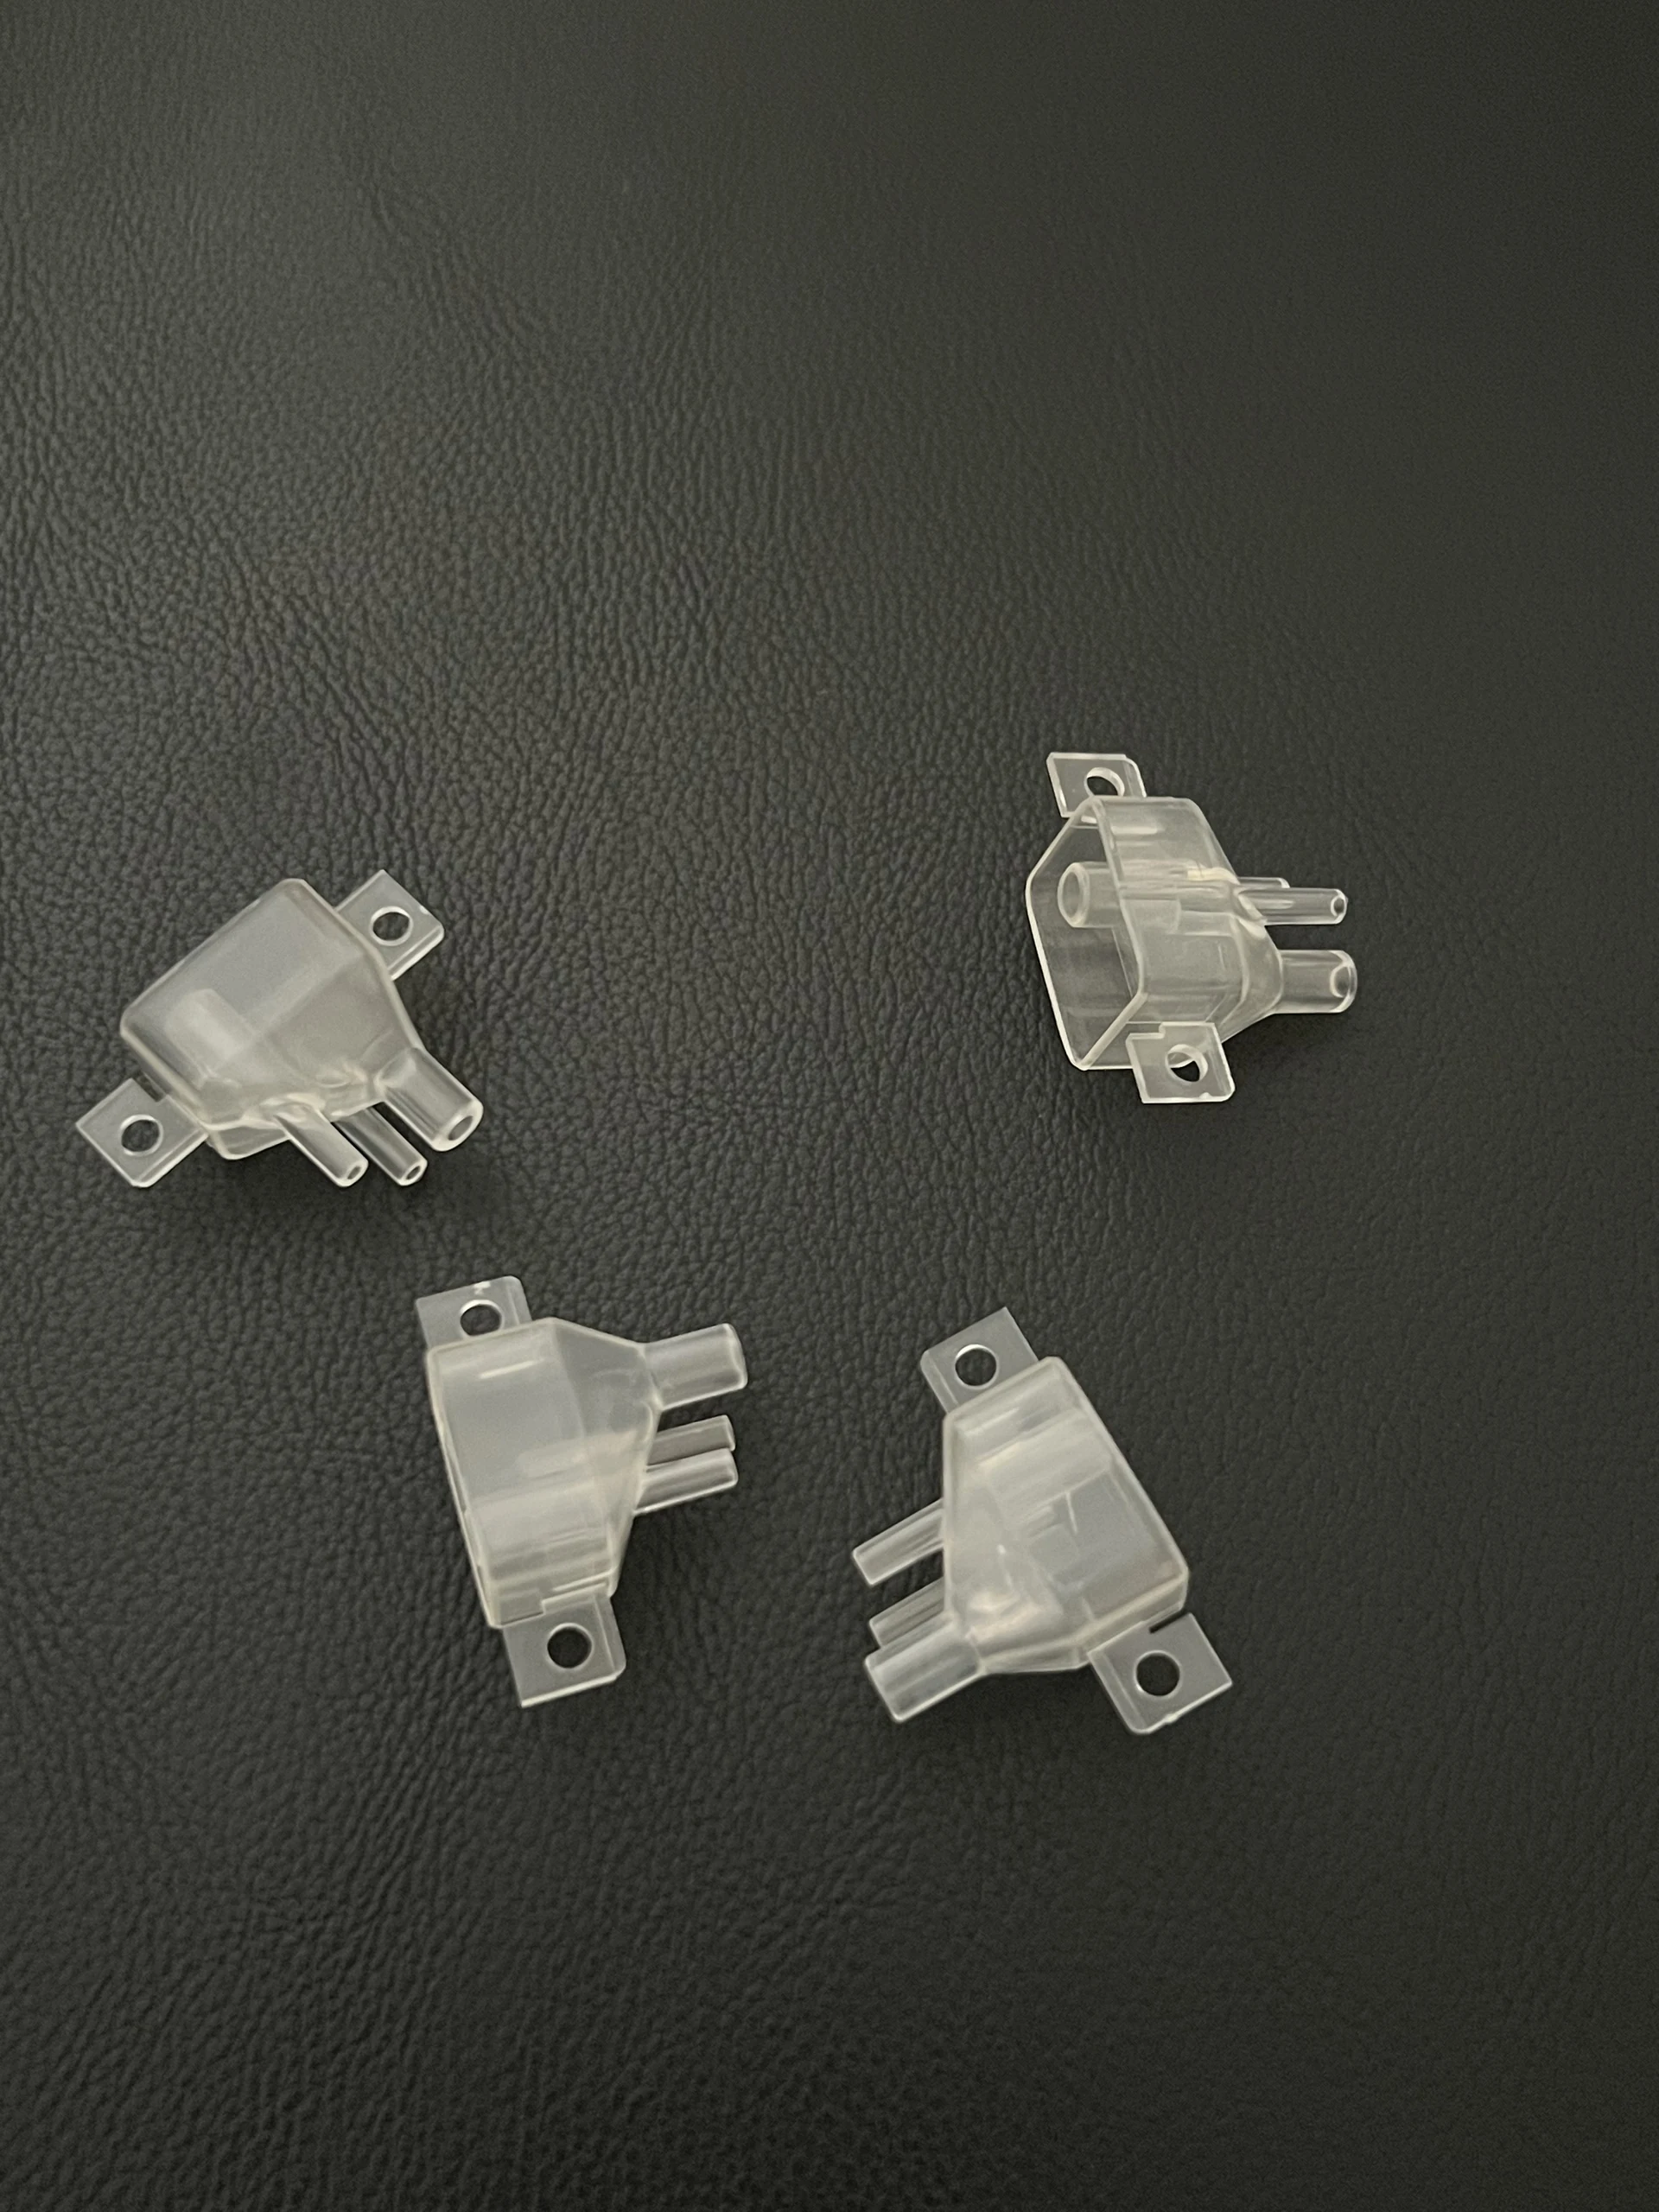
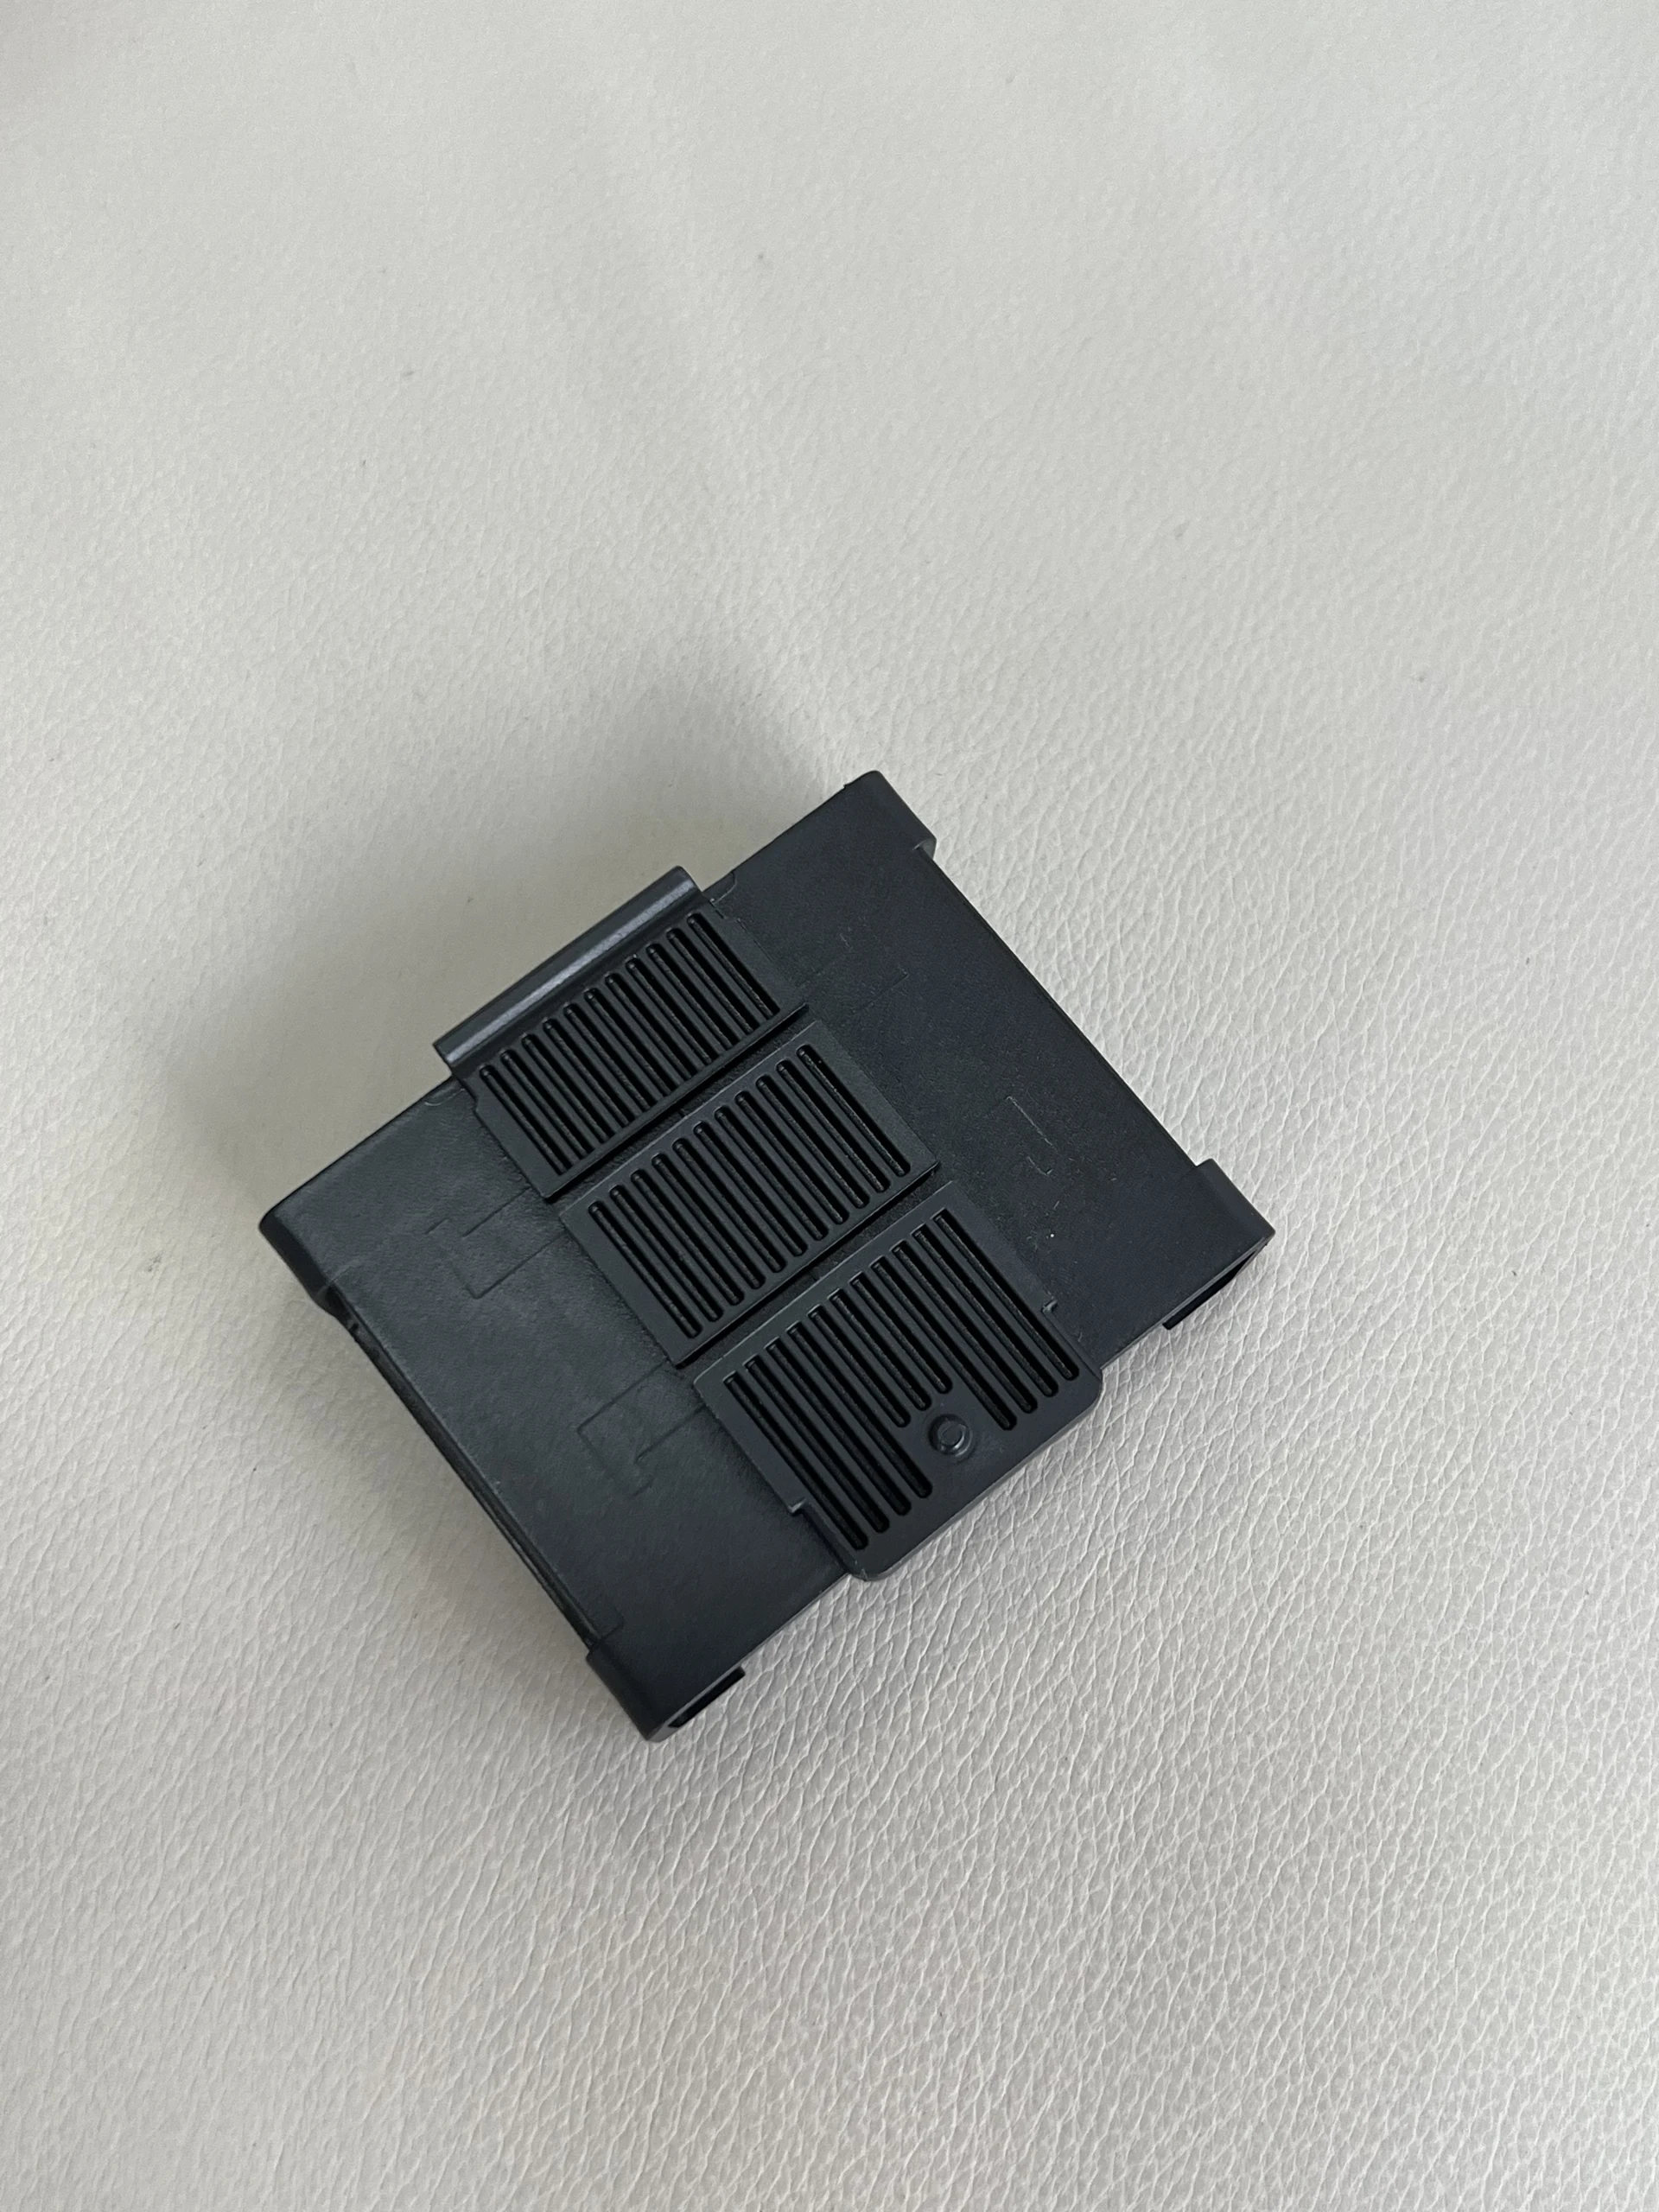
Precision plastic parts vary widely in shape and function, so a useful supply programme starts with a clear engineering brief rather than a generic accuracy claim. JingZhan supports tooling, injection moulding trials and repeat manufacture for custom structural and functional components. The examples below illustrate small moulded parts and ribbed housings; they are not a single standard product with shared dimensions or material. DESIGN AND MANUFACTURING Mark the dimensions that control fit, movement or locating accuracy. Define a datum system and measurement conditions, including any conditioning after moulding. Review the achievable tolerance feature by feature with the resin and geometry, rather than applying the same tight limit everywhere. Review ribs, bosses, corners and thickness changes before tooling. Include suitable draft and radii, and agree where gates and ejectors can be placed. The objective is repeatable geometry with acceptable appearance, not simply a mould that fills once. Provide temperature, load, chemical exposure and appearance requirements. Confirm the exact resin grade, colour and any restrictions on recycled content. Transparent, reinforced or textured parts need different processing and inspection decisions; the sample photographs do not establish those specifications. Inspect first articles against the agreed drawing and test fit with actual counterparts where practical. Record deviations and approved corrections. Release repeat production only when the customer has accepted the relevant dimensional, cosmetic and functional evidence for the defined scope. TECHNICAL SPECIFICATIONS PRODUCTION AND REPEAT SUPPLY The supplied manufacturing records include 50–500-tonne injection moulding machines and CNC/EDM tooling resources. Dimensional inspection equipment includes CMM, optical measurement and height measurement. Select a process and inspection route that matches the actual part: the availability of precision equipment does not mean every moulded feature carries the same tolerance or requires the same measurement method. Agree the drawing revision, resin grade, approved samples and critical-to-quality features before release. Record material lots and moulding conditions, inspect first-off parts and use cavity identification where specified. Define packaging, sampling and change approval so later deliveries can be compared with the same baseline. Tool maintenance and replacement inserts should be planned around actual production demand. Tooling investment is quoted separately from the piece price. Share annual demand and release quantities so cavity count, procurement and batch cost can be reviewed together. RELATED APPLICATIONS Structural supports, covers and locating components for electronic and industrial equipment assemblies. Small functional mouldings with openings, ribs, clips or other drawing-defined interfaces. Custom instrument components, including medical-equipment projects when their additional qualification requirements are separately defined. Application examples indicate possible engineering uses, not approvals or tested performance for every photographed part. Medical, electrical, flame-rating or chemical-resistance claims require the relevant grade documentation and project-specific validation. Discuss your drawing and supply requirements. Send CAD, resin preference, critical features, annual demand and release quantity. Contact our engineering team →Drawing-based precision plastic parts for ongoing supply
Key processing requirements
Put critical features ahead of blanket tolerances
Design sections for stable filling and cooling
Match resin and finish to the environment
Use trials to resolve assembly questions
Parameters agreed for your part
Parameter
Project specification
Manufacturing service
Custom mould development, injection moulding and repeat component supply.
Materials
Engineering thermoplastics selected against the project specification.
Geometry
Customer CAD and drawings; no common dimensions for pictured examples.
Tolerance
Feature-specific agreement based on geometry, resin and inspection method.
Surface finish
Colour, texture and permissible moulding marks defined by zone.
Tooling
Cavity layout, inserts and expected demand reviewed before quotation.
Inspection
First-article report and agreed batch sampling or gauges.
Packaging
Part protection, quantity per pack and lot identification to customer needs.
Equipment, lead time and order planning
Planning item
Basis for quotation
DFM review
Indicative 3–5 working days after complete drawings and requirements.
New tooling
Indicative 4–8 weeks to first tool trial after tool-design approval and commercial release; corrections and customer validation are additional.
Order quantities
Initial quotation-planning basis: a 500-piece pilot or 1,000-piece repeat batch per part number, resin and colour, subject to project quotation.
Repeat orders
Indicative 10–15 working days after materials and the production slot are confirmed. Customer qualification, special processing and transit are additional.
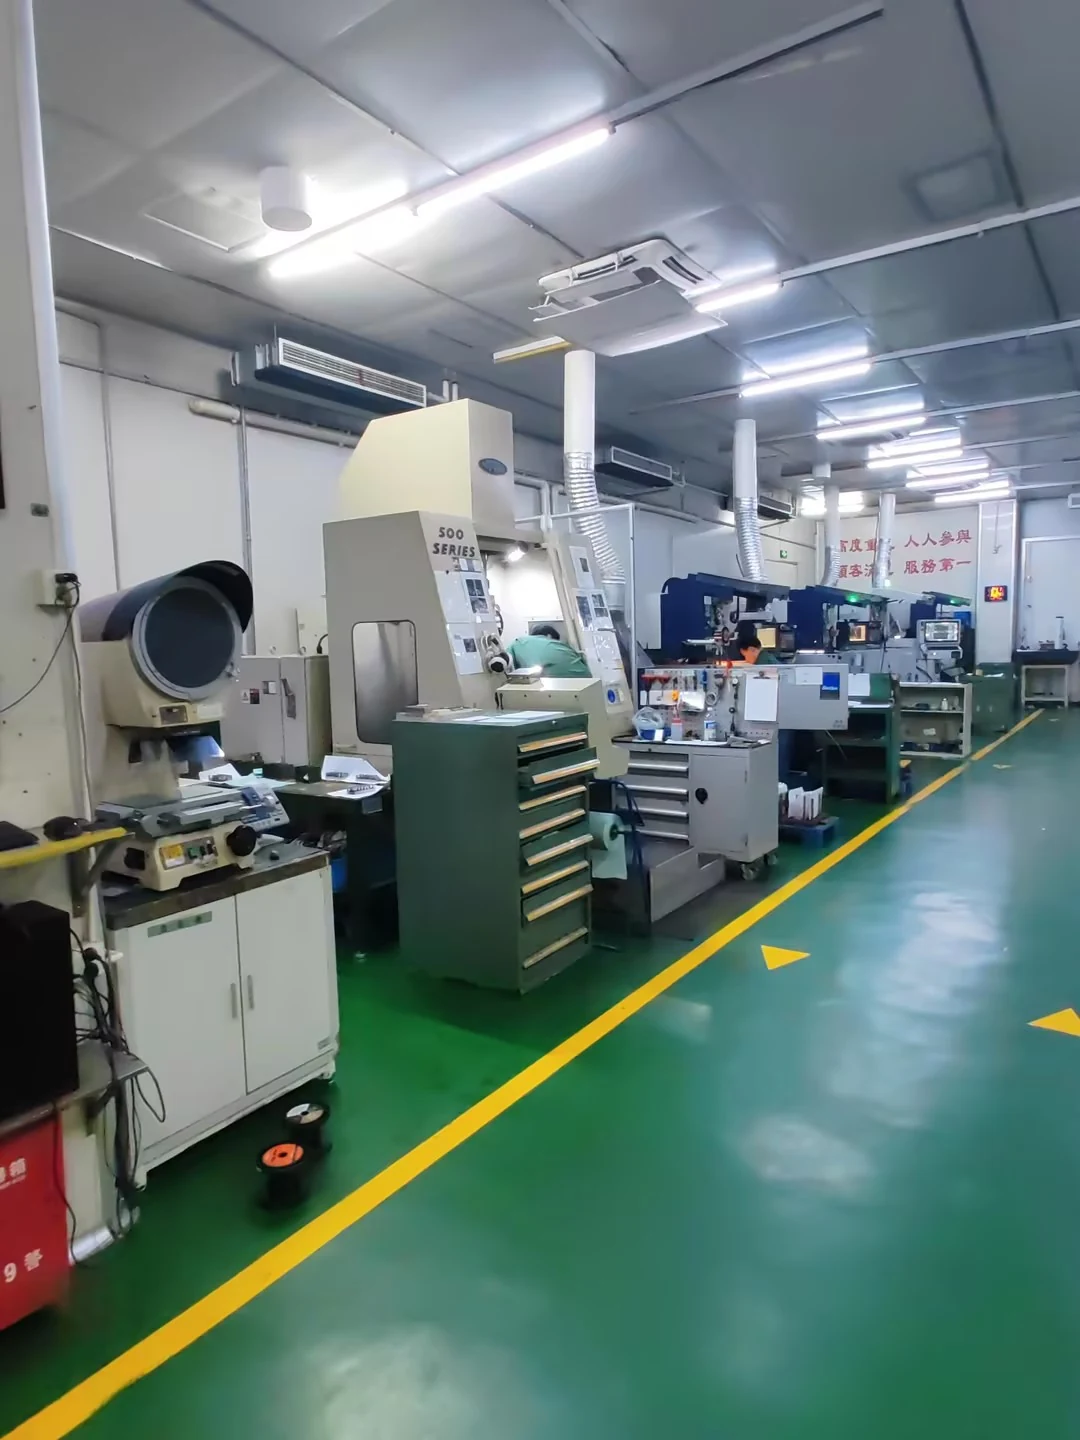
Keep repeat orders on an approved baseline
Where these components can be used
Technical Specifications
Our injection molding capabilities cover a wide range of materials, part sizes, and complexity levels. Below are the detailed technical parameters.
| Clamping Force | 80 1,600 tons |
| Max Part Weight | 0.1g 6,000g |
| Max Part Dimensions | 1,200 脳 800 脳 400mm |
| Injection Pressure | Up to 2,500 bar |
| Mold Materials | ABS, PC, PP, PA66, POM, PEEK, PMMA, TPE, etc. |
| Mold Life | 500,000 2,000,000 shots |
| Lead Time | 150 working days (T1 sample) |
| Certification | ISO 9001:2015, IATF 16949, ISO 13485 |
| Special Processes | Insert Molding, Overmolding, Two-Shot Molding |
Recommended Products
Explore our high-precision injection moulded components trusted by industry leaders worldwide.